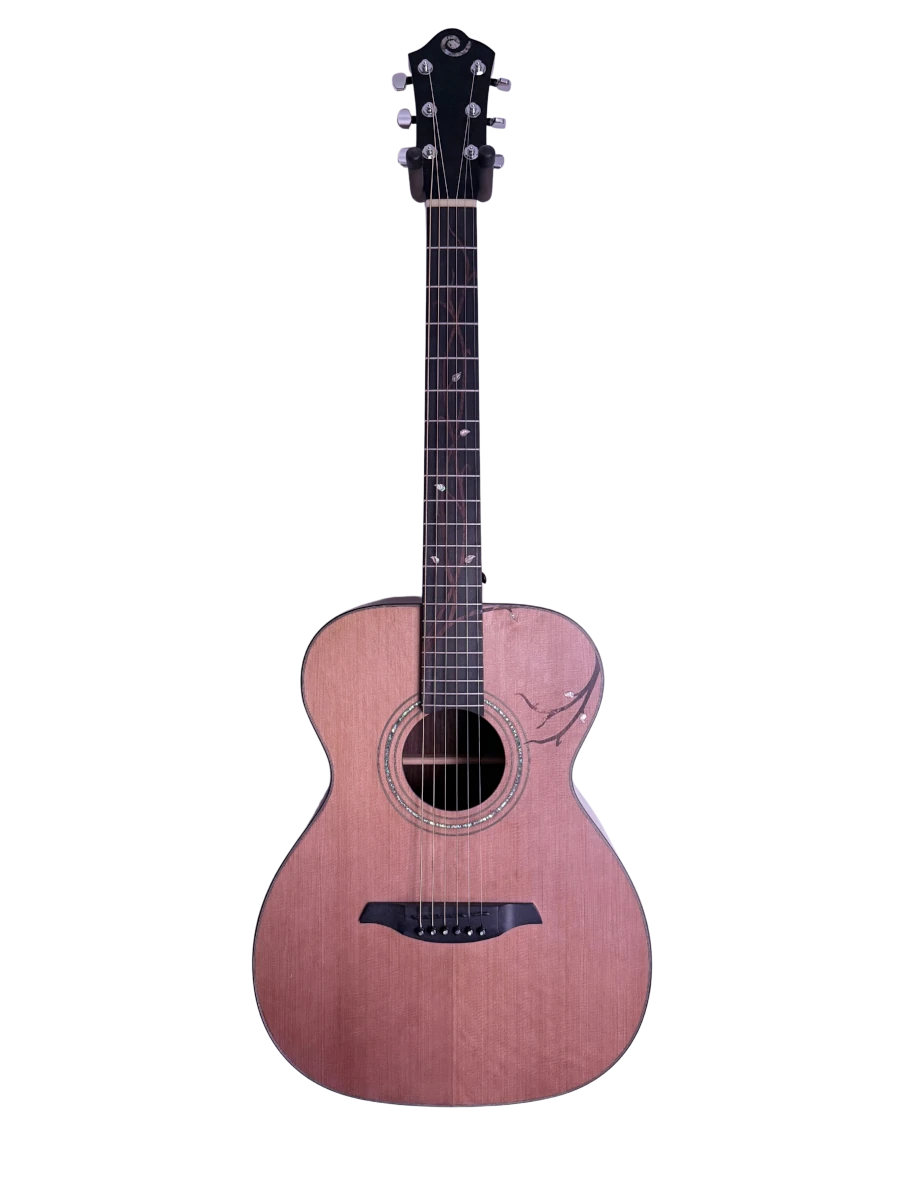
The Continental features an OM body shape, has a center soundhole, solid Rosewood back and sides, a Western Redcedar soundboard, solid wood everywhere (no laminates) and even includes a truss rod!
The body is a bit deeper than conventional, being 4" deep at the neck block and 4-5/8" deep at the tail block. The soundboard bracing is Sitka Spruce, but the pattern is a double-X.
On this particular build, an unfortunate accident that resulted in an ugly, unrepairable ding in the soft Cedar soundboard inspired additional soundboard inlay.
On this page
- Specifications
- Plate Joining
- Kerfed Lining
- The Back
- The Blocks
- The Soundboard
- Closing the Box
- Binding and Trim
- The Neck
- The Fretboard
- The Truss Rod
- The Mortise and Tenon
- Completing the Neck
- Decorative Purfling
- The Headstock
- Recovering From Damage
- The Bridge
Specifications
- Model: Continental
- Body Style: OM (Deep Body)
- Upper Bout: 11.25″
- Waist: 9″
- Lower Bout: 15″
- Body Length: 19.25″
- Body Depth (Tail block): 4.625″
- Body Depth (Neck block): 4.0″
- Scale Length: 24.9″ (632.5 mm)
- Nut Width: 1.75" (45 mm)
- String Spacing: 2-1/4"
- Soundboard: Western Redcedar
- Back and Sides: East Indian Rosewood
- Bracing: Adirondack Red Spruce
- Bracing pattern (Back): Conventional ladder
- Bracing pattern (Soundboard): Double-X
- Binding: Gabon Ebony
- Soundhole Binding: Indian Rosewood
- Rosette: Paua
- Neck: 5-piece Mahogany
- Fretboard: Gabon Ebony
- Fretboard Inlay: Mahogany and Paua
- Headplate: Gabon Ebony
- Bridge: Gabon Ebony
- End graft: Gabon Ebony
- Tuners: Sperzel Open-back Trim-lok
- Options: Soundboard Inlay
- Weight: 4.45 lbs (with tuners, strings, pickup)
Plate Joining
There was a time when trees that would be large enough in diameter to fashion a large guitar’s soundboard or back entirely from a single slab or billet of wood were in plentiful supply. Within the last century, as large trees were harvested faster than they were re-planted, the option of beginning with a single, massive plate of wood began to quickly disappear.
Regardless of availability, the potential for splits across that large of a span of wood due to seasonal or environmental movement could be mitigated by ripping large plates lengthwise and rejoining them, improving their stability.
Book matching, the practice of slicing two (2) adjacent plates (from the same half of the tree), laying them open like a book, and joining them opposite a center seam (creating a mirror image of the grain pattern) proved to be more structurally sound, more popular and more aesthetically pleasing than looking at a single, large cross-section of a tree.
I used a plate joiner jig to glue two (2) book matched halves of the Cedar soundboard of this deep-bodied, OM-sized guitar together. The two (2) book matched halves that make up the Rosewood back were assembled in the same manner.
In a practice shared throughout lutherie, two (2) boards are matched, planed or sanded down thinner than when we started (we say, "thicknessed", while we mean "thinned"), glue is applied to the edges to be joined, and the boards are assembled into some clever contraption which pulls them tightly together with very even pressure while preventing them from buckling as the glue dries.

Kerfed Lining
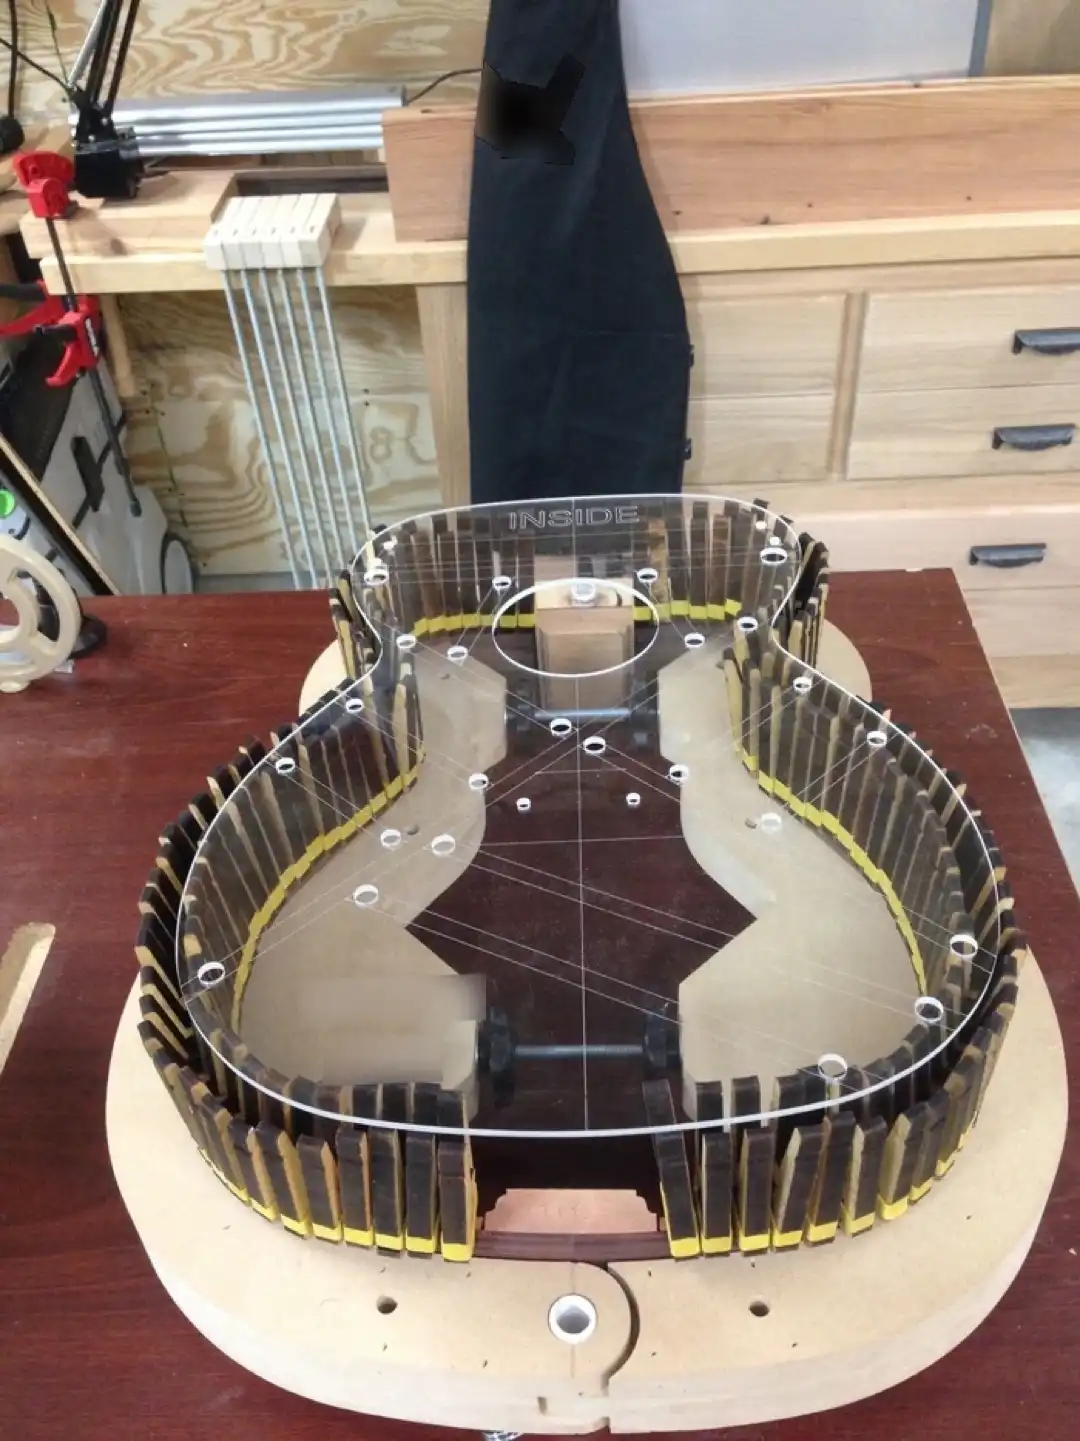
I bent two (2) Rosewood sides and held them in a form (a "body mold") while I attached a Mahogany neck block and a tail block. This forms the basis of a frame, or "body shell" onto which the back plate and the front plate ("soundboard") will be joined.
The intersection of the back plate and the rims of the sides is worth mentioning. Guitars made of all-carbon fiber are able to unify a front plate and back plate directly with the sides, forming an impressively strong and rigid box that is often stunningly attractive in appearance.
Attempting to join thin, wooden plates in similar fashion is not pragmatic. To create a bond sufficient to hold the pieces together, epoxy is necessary. Any efforts to soften (radius) the sharp outside edges that are formed weakens the bond. Those edges are readily subject to damage. The abrupt transition between planes (especially that of the sides and the soundboard) is generally considered to be visually unattractive.
A lightweight ledge must first be formed along the inside edges of the sides, a "rim" onto which the back and the soundboard can be confidently attached using wood glue. This ledge is just large enough to both support the joining of the sides and the plates, while allowing for the addition of binding along with (if desired) decorative purfling.
The ledge is commonly formed using a strip of wood into which multiple saw cuts ("kerfs") are made, perpendicular to the length of the strip of wood. By stopping just shy of sawing all the way through the wood, an easily bendable component is created, one that can follow the curves around the the rims of the body.
Kerfed lining strips are readily available in lightweight hardwoods such as Mahogany or Basswood, but can be made from most anything. Traditionally, the saw cuts were positioned away from direct contact with the side, being visible when viewed through the soundhole. With a slight design change, so-called "reverse kerfed lining" is installed by gluing the open saw cuts to the wood of the sides, resulting in a more finished appearance.
On two (2) identically-sized bodies, reverse kerfed lining will slightly reduce the area of the open soundboard when compared to standard kerfed lining. It is commonly belied to result in a bit more rigid body shell. Reverse kerfed lining is my personal preference between the two.
The Back
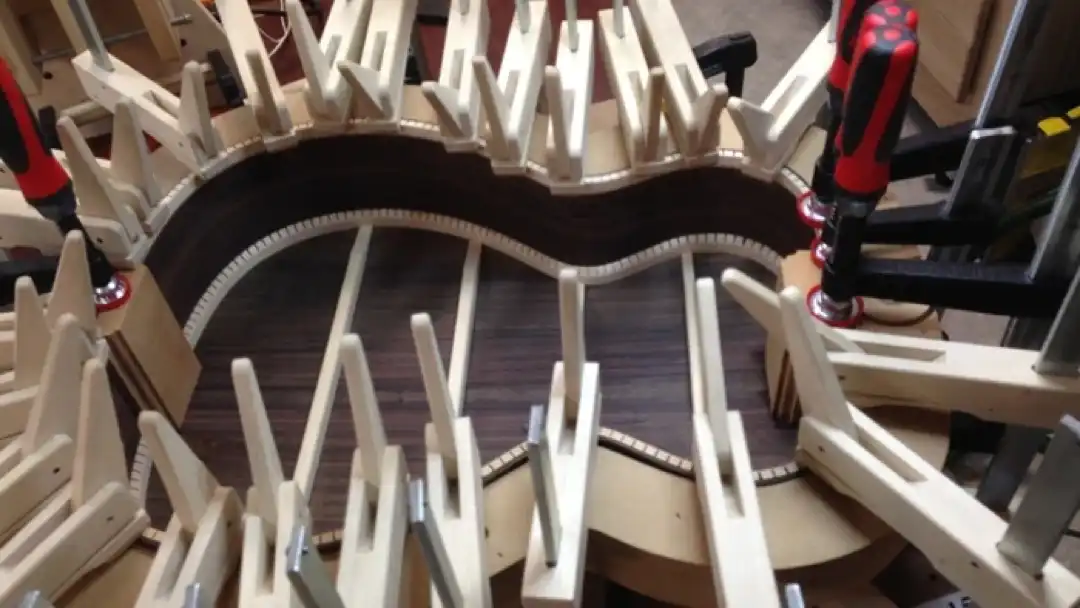
Stout braces were added to the Rosewood back in a traditional "ladder" pattern. The conventional center graft was intentionally omitted. I am only able to demonstrate performance over ≈ 20 years, not 60 or 80 years, but I am of the opinion that, with the advent of modern glue(s) and proper clamping, back plate center grafts serve little purpose but to add weight.

The back was joined to the sides (one simply cannot have too many clamps, can one?).
The Blocks
A view of the tail block shows a recess that has been drilled to reduce the thickness of this otherwise hefty tail block. This area gets drilled later to receive a strap jack. It could receive a traditional end pin, just as easily.

This view of the neck block shows the two (2) recessed holes for the bolts used to secure the neck to the body. Bolt-on neck attachment is common, these days, but still raised eyebrows back when I built this guitar.

The Soundboard
The Western Redcedar that I selected for the soundboard was cut 30 years earlier from a tree that was more than two hundred years old! It is stiff, among the stiffest I have encountered. Often, Cedar will be exceptionally stiff along the grain, even rivaling Spruce, though it tends to be weaker across the grain.
As a result, many builders will leave Cedar Soundboards a bit thicker than their Spruce counterparts to make up for the difference. Occasionally, one may encounter some really special wood that can be thinned a little more than the rest. I have high hopes for this guitar!
I routed the purfling and Paua soundhole rings using a rotary tool mounted in a mini router jig and attached to a circle cutter. After the inlay work was complete, I cut a circle all the way through the soundboard, creating the soundhole.
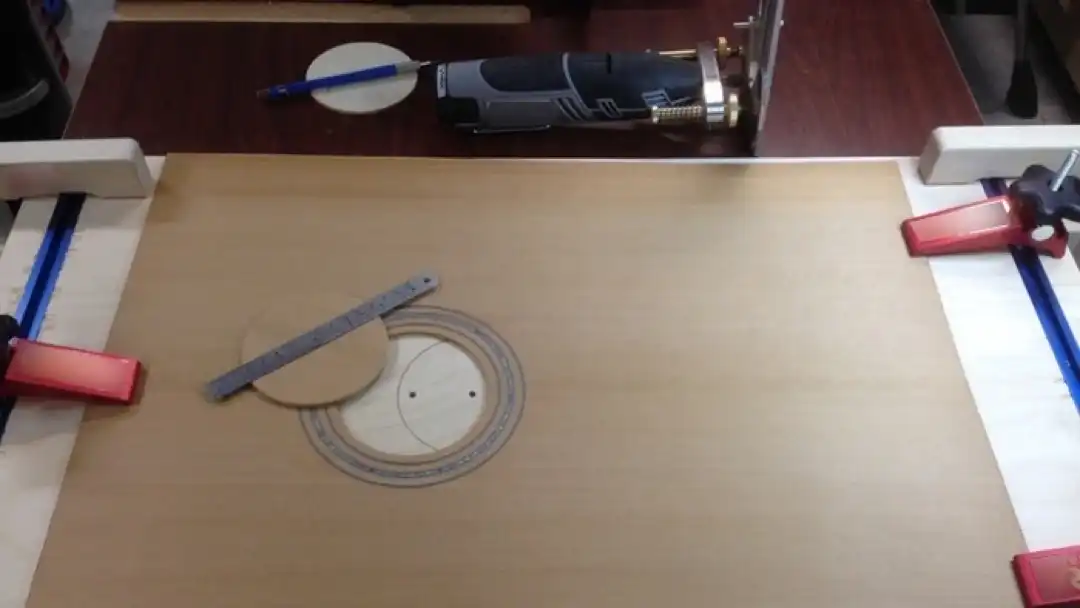
A close-up image highlights the attractiveness of the combination of Cedar, Paua, and black-white-black (BWB) purfling circling the soundhole, forming a series of decorative concentric rings that are often referred to collectively as a rosette.

Perhaps more significant than materials, dimensions, and patterns, soundboard and bracing stiffness largely determine the overall output of the acoustic guitar. I chose to employ a progressive double-X bracing pattern. I wanted to coax the brightness out of this top, and I have found the double-X pattern to be very suitable for the task. To maximize volume, I will keep the soundboard at a relatively flat 50 ft radius. The additional “X” below the bridge will add the extra support where it’s needed, especially for this flat of a top.
Near the center of the lower bout of the soundboard, directly beneath the bridge, lies the bridgeplate. There has been speculation that this thin piece of material (traditionally, Rosewood or Maple) became popular among luthiers during the advent of the ball-end steel strings, as the steel ball would quickly chew through the softwoods traditionally used for the soundboards. Maple, though softer, is thought to lend a "brightness" to the overall sound, while Rosewood is "oily and tough," a good choice to resist the wear from the metal.
Early in my lutherie adventures, I had a wild thought: Why not use both woods, and benefit from each wood's contribution? I began laminating Maple and Rosewood for my bridgeplates, usually positioning the Maple against the soundboard. With the stiffness of the top, and the addition of the double-X pattern, the last thing I need is significantly more brightness. Here, I will simply use a solid Rosewood bridgeplate.
In addition to its "resist-the-metal" role, as well as its "sonic enhancement" role, the bridgeplate effectually sandwiches the soundboard between itself and the bridge, and assists in keeping the soundboard flat(-ter) in this critical area. The idea is to mitigate the potential of the bridge to simply peel off the soundboard as a result of string tension.
Undersized or overly-thin bridgeplates can accompany guitars having most impressive low frequency response (lots of bass), though that may be short-lived. These soundboards often begin to pull, or belly, upwards. That is not necessarily a problem, tone-wise, but it can present a major challenge in maintaining playability.
The angle at which the plane of the fretboard encounters the (approximate) plane of the contoured/radiused soundboard must be optimized to prevent the strings from either lying on the frets or standing too far off the frets. Guitars that belly (pull upward due to string tension) significantly typically end up requiring early neck resets, as the strings eventually rise too high above the fretboard for comfortable playing, and no amount of saddle height adjustment can correct the problem. They may sound great, but they are no fun to play!
Rapid bellying after initial construction is typically evidence of some combination of insufficient soundboard stiffness, bracing strength, and bridgeplate size.
Conversely, too large a bridgeplate is a real tone killer (as is too thick or too stiff a soundboard, along with too much bracing). Sizing a bridgeplate incorrectly can critically impact the performance of the instrument.
While arguably sacrificing some lower frequency response, leaning slightly toward a larger plate versus a smaller plate provides the peace of mind that the soundboard will stay where it belongs over time.
The two (2) materials expand and contract at different rates. A hopeful function of the fretboard patch, which is applied to the backside of the soundboard, has been to minimize the soundboard’s contraction and expansion at this critical juncture. In the case of this guitar, the fingerboard extension is not glued but rather secured to the soundboard using a small bolt. The epoxied carbon fiber provides something more significant than soft Cedar to support a washer and nut.
he two (2) materials expand and contract at different rates. A hopeful function of the fretboard patch, which is applied to the backside of the soundboard, has been to minimize the soundboard’s contraction and expansion at this critical juncture. In the case of this guitar, the fingerboard extension is not glued but rather secured to the soundboard using a small bolt. The epoxied carbon fiber provides something more significant than soft Cedar to support a washer and nut.

The objective with bracing is to support significant string tension while allowing the soundboard to vibrate as freely as possible from the plucked strings' energy. It is a delicate balance: An over-braced soundboard results in a rather dull, lifeless guitar, as the strings must be strummed or plucked hard in order to generate any front plate vibration which, in turn, is dampened by all that bracing. An under-braced soundboard can result in a collapse or implosion, though it will likely sound wonderful during it’s short life.
The braces were glued onto the soundboard as long, thin interlocking rectangles, and then scalloped and shaped in place with a chisel. Some careful sanding dressed them up for final presentation. Of note, this particular bracing profile happens to resembles duck heads or bottlenose dolphins.

Closing the Box
All four (4) braces on the back plate, along with the primary X-brace and transverse brace on the front plate, are deliberately left longer than the dimensions of the body. The sides will be notched to receive these "through braces", allowing the ends of these braces to rest directly on the sides.

I reinforced the guitar’s sides with very small, lightweight braces.

Once the soundboard was fitted to rest flush against the body, I glued it in place.
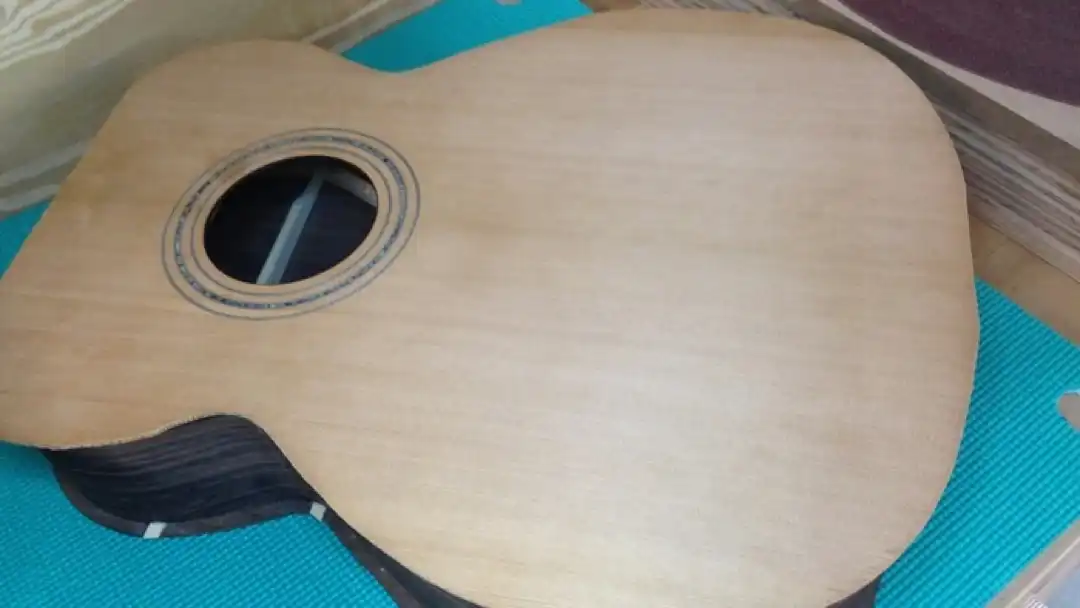
Binding and Trim
A decorative plate known as an end graft is often added to the tail end of the guitar, spanning what would be the seam formed by the two (2) sides butting together at the tail block. This wooden wedge provides for a visually pleasing break in the seams of the guitar sides as well as eliminating the need to perfectly align and match the grain of the two (2) sides. Even when sides are matched correctly, without an end graft, there exists the possibility of appearing like something is missing or was forgotten.
Extra attention is paid to centering the soundboard on the centerline of the body. I nailed the center seam, which is near invisible. But you would never know it without a very close inspection. Humorously (aggravatingly), a dark grain line mocks my effort, displaying prominently just 1/32″ off center (on the treble side), from where the two (2) halves of the front plate join. I did it right!, No, really!
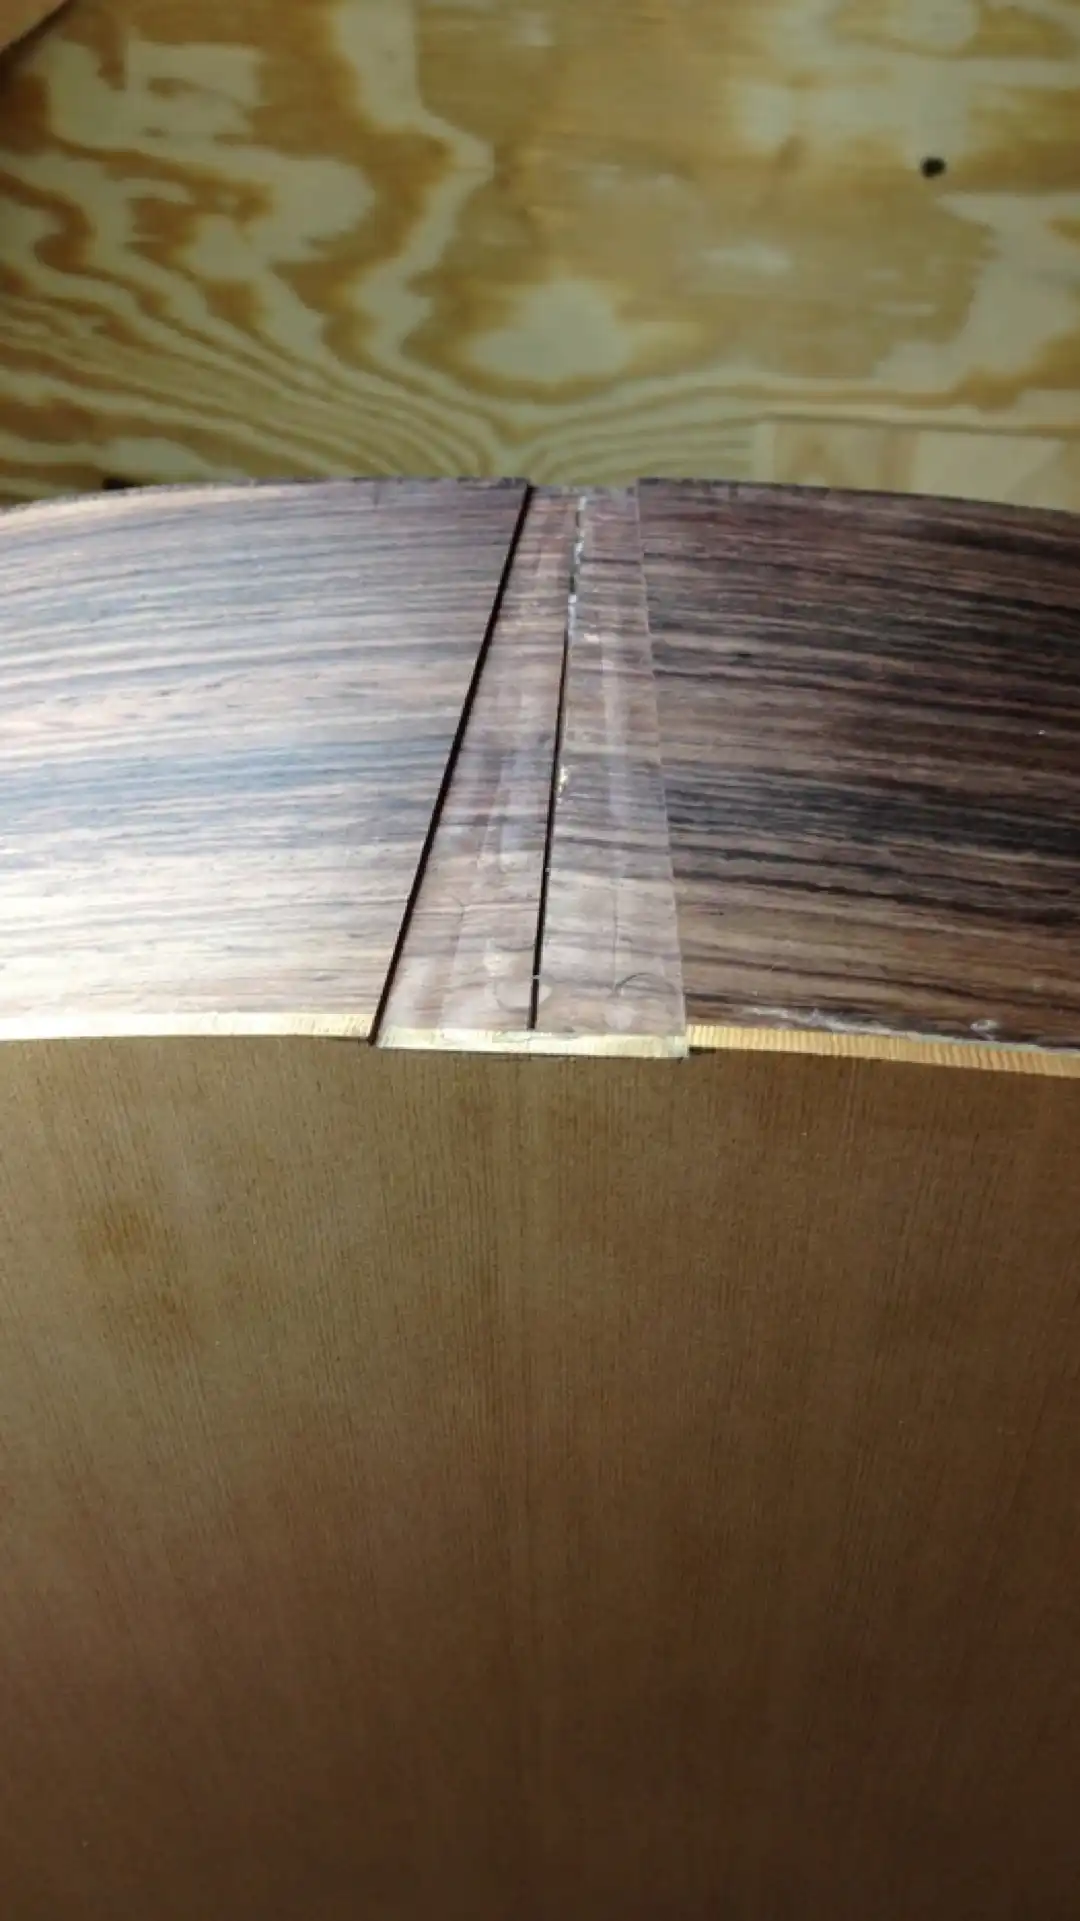
The Ebony end graft installed, and scraped smooth.

The Neck
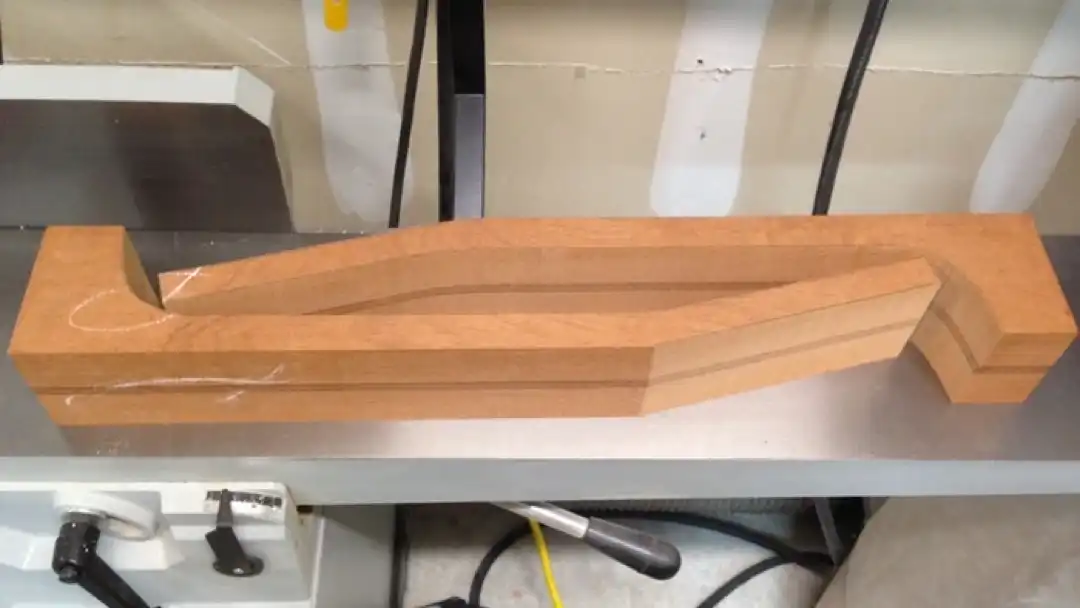
Most all of my necks are 5-piece laminated for increased stability as well as visual interest. The blanks are resawn from large billets, planed and glued back together with three (3) wood center strips. I can cut two (2) necks from one of these laminated blocks of Mahogany.
If there is a downside to this approach, it is related to the use of that chisel. To mitigate "splitting" already glued-on braces (a "no-no"), you need razor sharp chisels. If you "slip" with one of those razor sharp chisels, it is easy to gouge the soundboard, or worse.
Not everyone feels the need to embellish the shape of their headstock, but I always have. A distinct shape can be readily identified with the builder, and provides an opportunity to be creative. I worked diligently to produce a unique, yet simple design, one that both honored the instruments that inspired my efforts, and let me make my own statement. The crest atop the headstock is all Cozad Guitars!
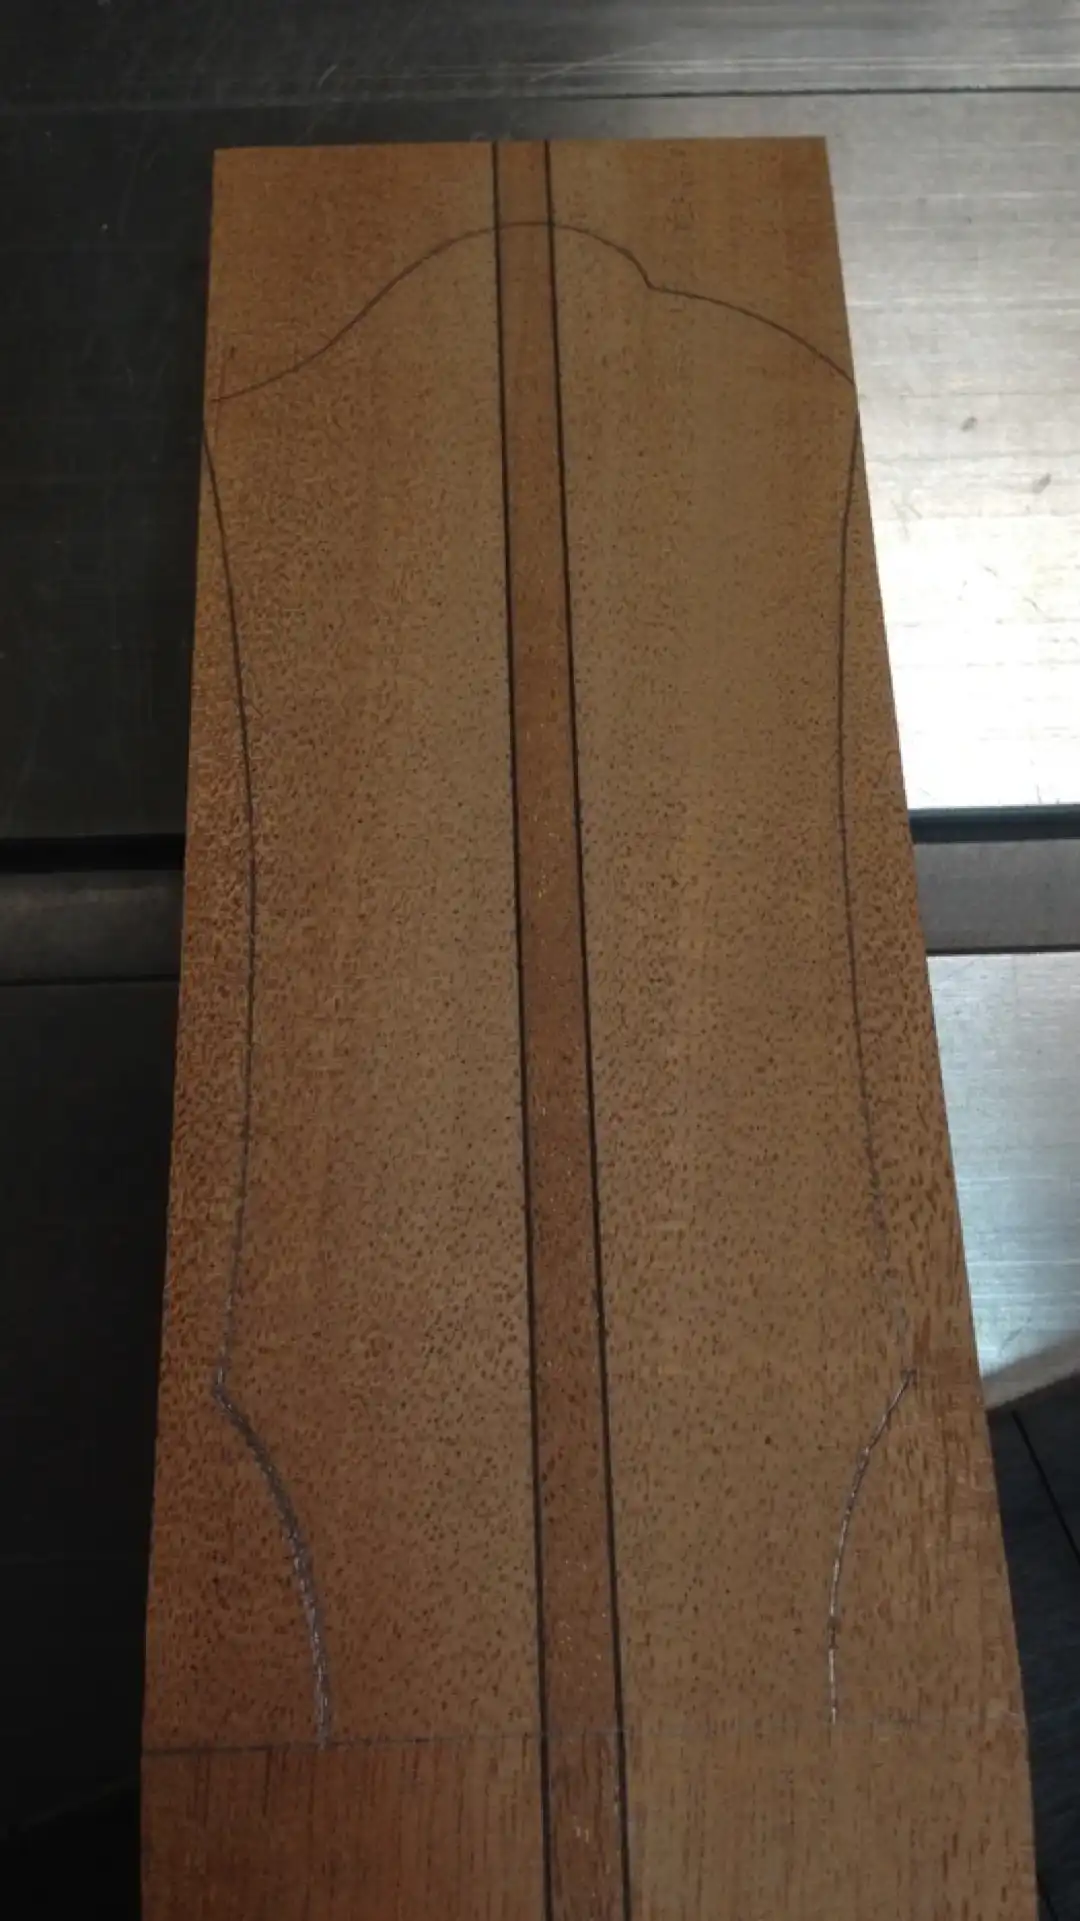
The two (2) most basic components of the modern steel string acoustic guitar, the neck and the body.

The Fretboard
Starting with an Ebony blank, I squared it, thicknessed it, slotted it to my target scale length, radius it and inlay it.
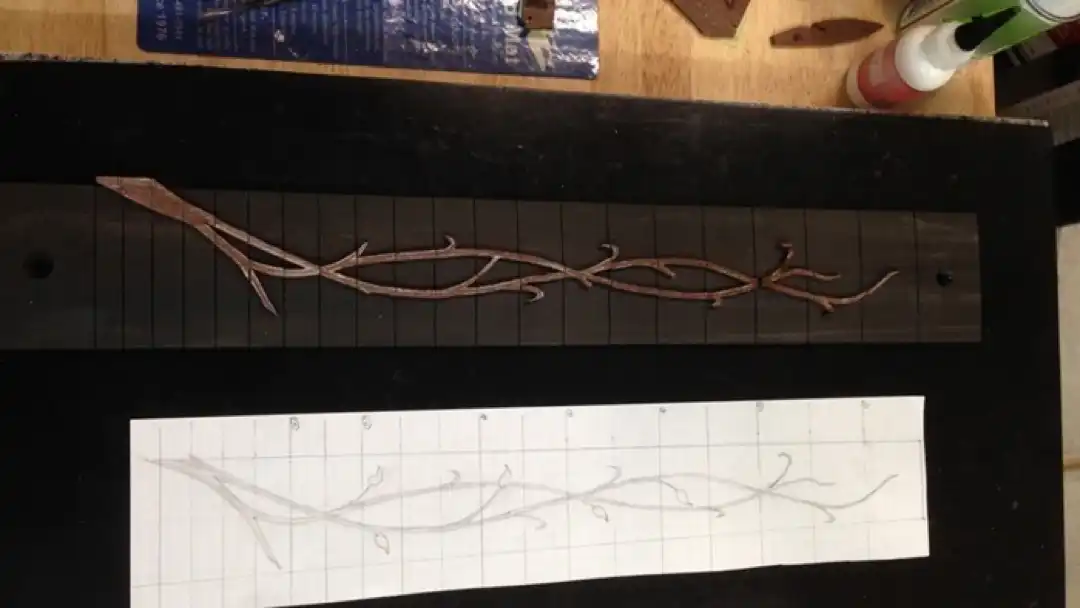
I had sketched an idea on paper that I wanted to inlay into the fretboard.

After transferring the drawing to wood, I cut out the shapes by hand. The "vine" was fashioned from a single piece of mahogany using a jeweler’s saw.

Many people are intimidated by the perceived degree of difficulty of this type of work. In no way do I mean to under-value the art form of inlay when I say that it is often tedious, but it is not always difficult. Attention to detail, patience and a steady hand are required.
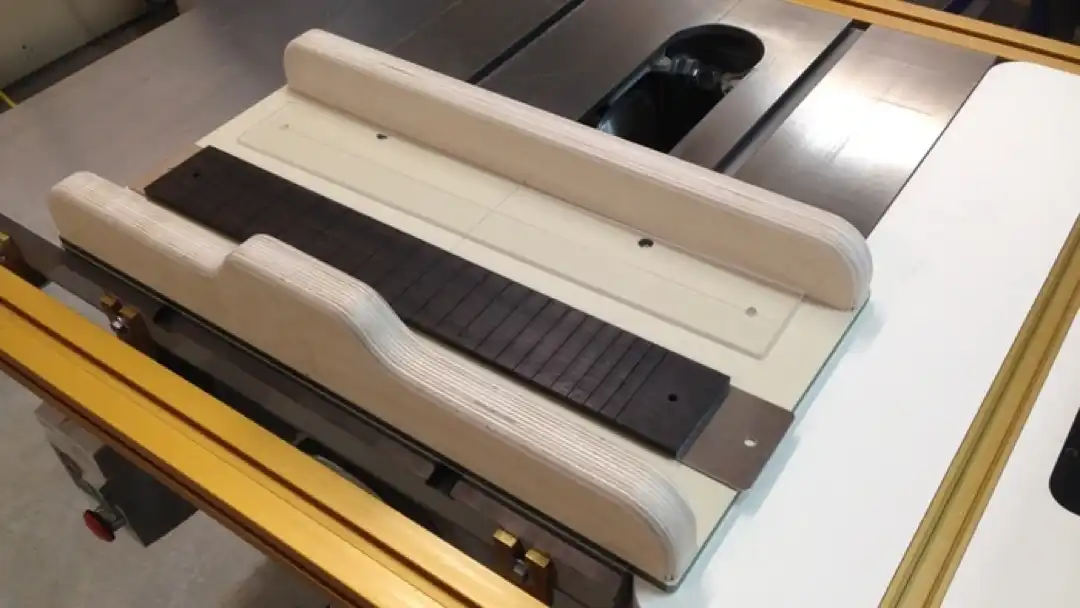
If inlaid pieces are primarily located down the center of the length of the fretboard, inlay work can be completed prior to radiusing its surface. However, that can be dangerous for inlay that spans the width of the board, which is the case, here. I radiused the board, first, by mounting it to a jig which I passed it through a drum sander several times, rotating the fretboard along it’s length on each pass. After radiusing, the fingerboard was routed to receive the inlay.

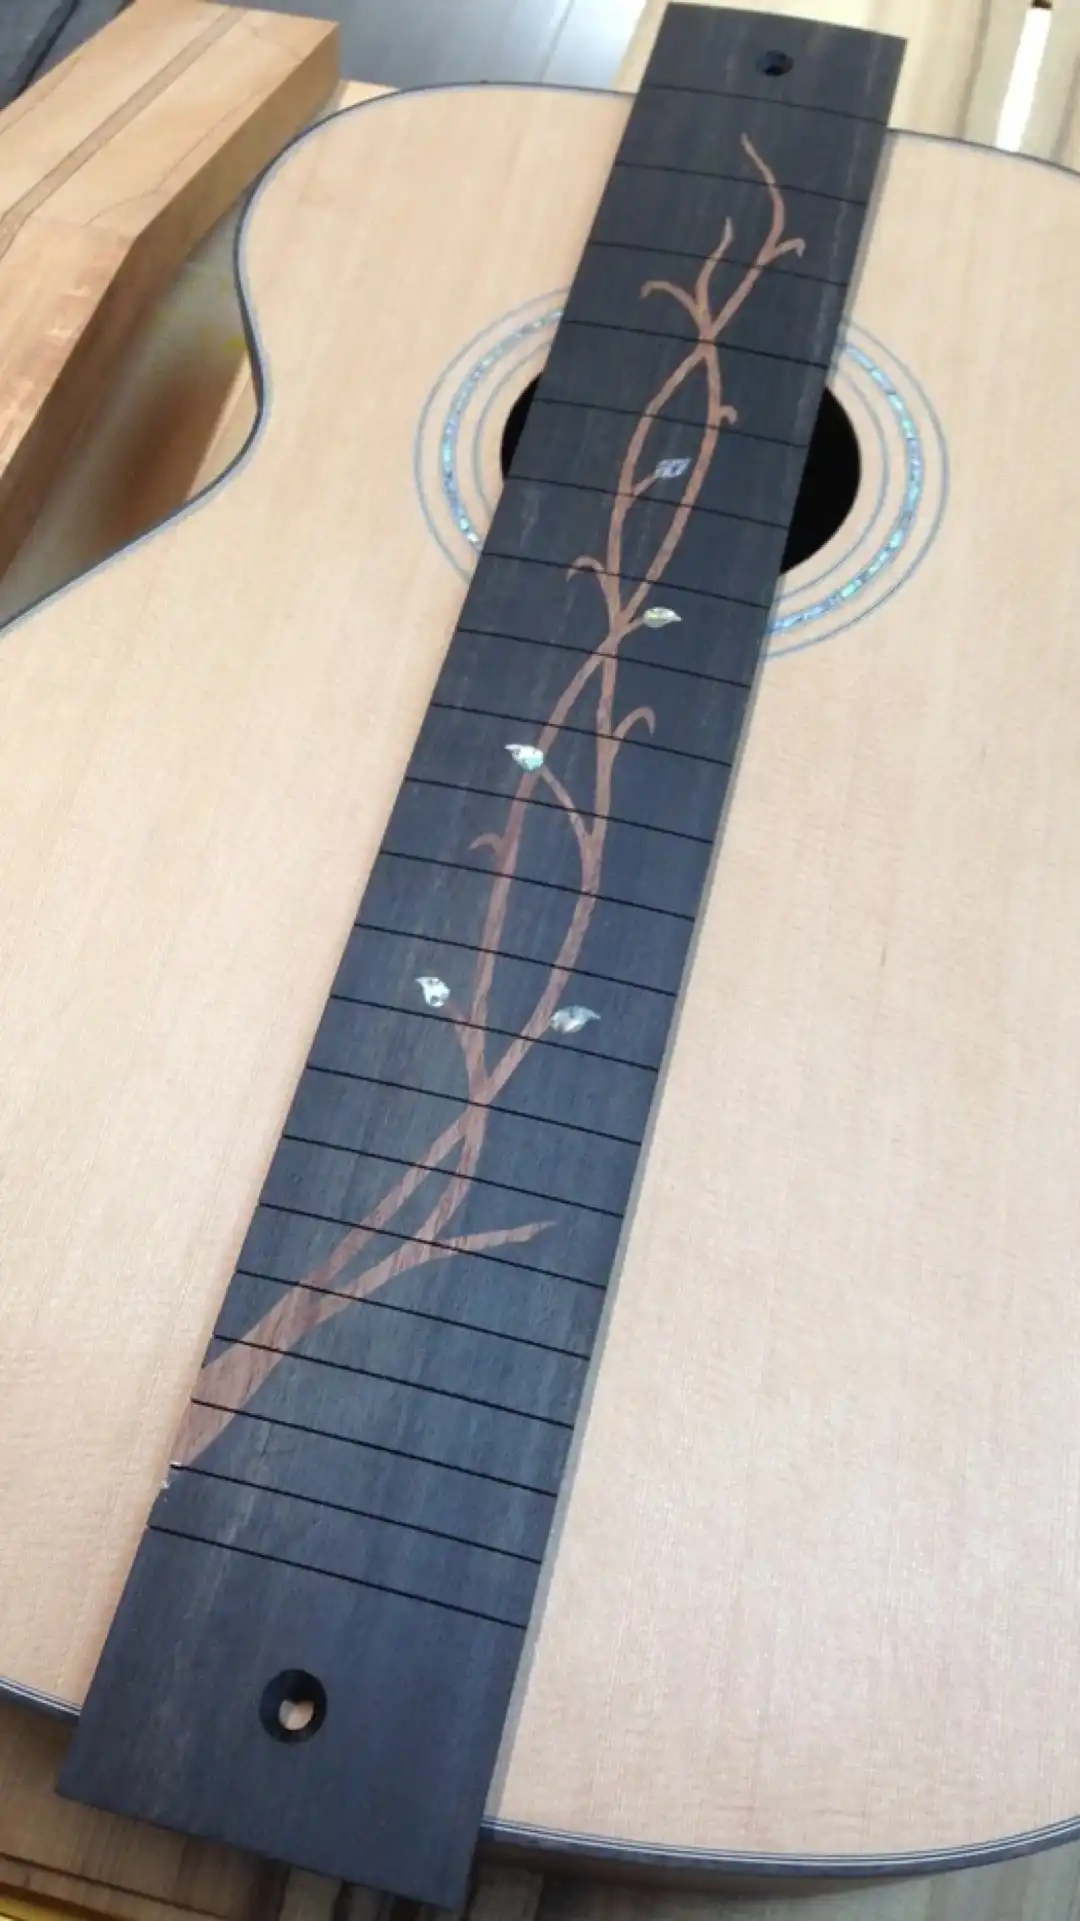
I cut several small florets from Paua and inlayed them into the fretboard along with the mahogany vine. The placement of the florets is not accidental. These are fret markers, and provide the player with a quick visual reference for finger placement.
Many people are intimidated by the perceived degree of difficulty of this type of work. In no way do I mean to under-value the art form of inlay when I say that it is often tedious, but it is not always difficult. Attention to detail, patience and a steady hand are required.
The Truss Rod
The neck gets stiffened using two (2) carbon fiber rods.
Having constructed a number of necks, using a number of methods, both with and without carbon fiber, and both with and without truss rods, I have developed my own preferences.
My "favorite" neck stiffening solution relies solely on a carbon fiber D-Tube from DragonPlate. If, in lieu of the D-Tube, I am wanting to incorporate a truss rod (eg, to satisfy a specific Client's request), then I will add carbon fiber to the neck, as you see here.
I believe the addition of carbon fiber to the neck is beneficial in more than one way. It adds torsional stability and is typically lighter than the wood it replaces. In the case of my D-Tube necks, I have no doubt that they contribute to an overall "brighter" response and greater sustain. Supplementing a truss rod with carbon fiber stiffeners most assuredly can strengthen an otherwise weak area beneath the nut.

The Mortise and Tenon
A mortise is cut into the body of the guitar using a plunge router. A router jig and template, called an edge vise, is used for exact positioning. This tool is used in conjunction with a precision neck angle jig.


This neck is held to the body using two (2) socket head cap screws, wavy washers and steel cross dowels (threaded inserts may be used in place of cross dowels, if desired, and are lighter in weight).
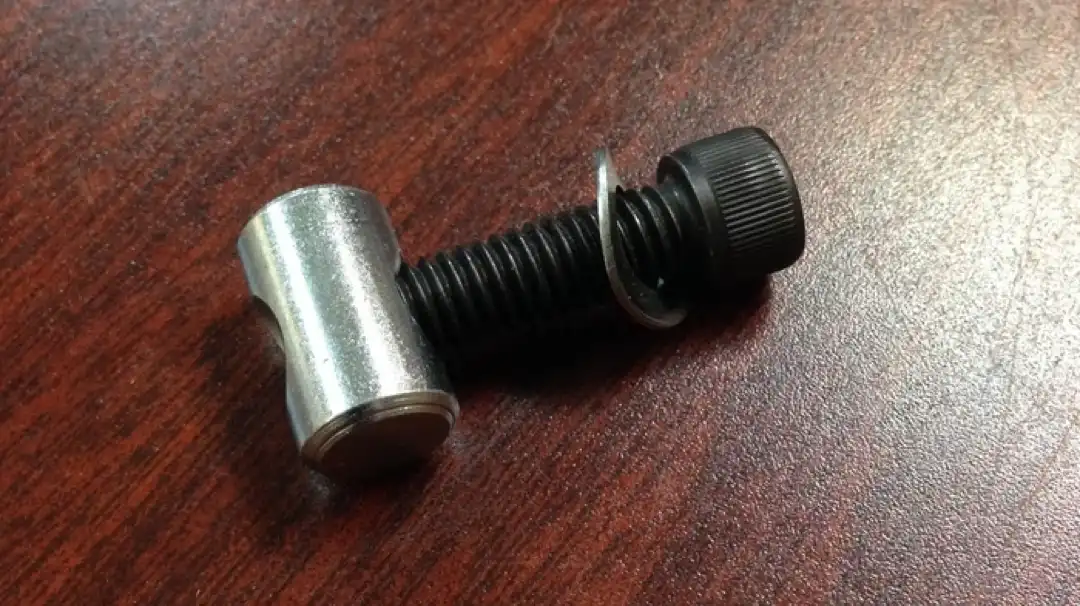
Holes are drilled in the neck, prior to cutting the tenon, in order to house the cross dowels.

The neck is then clamped into the neck angle jig where the tenon is cut using the same plunge router that cut the mortise. The angles of the cuts are very important.
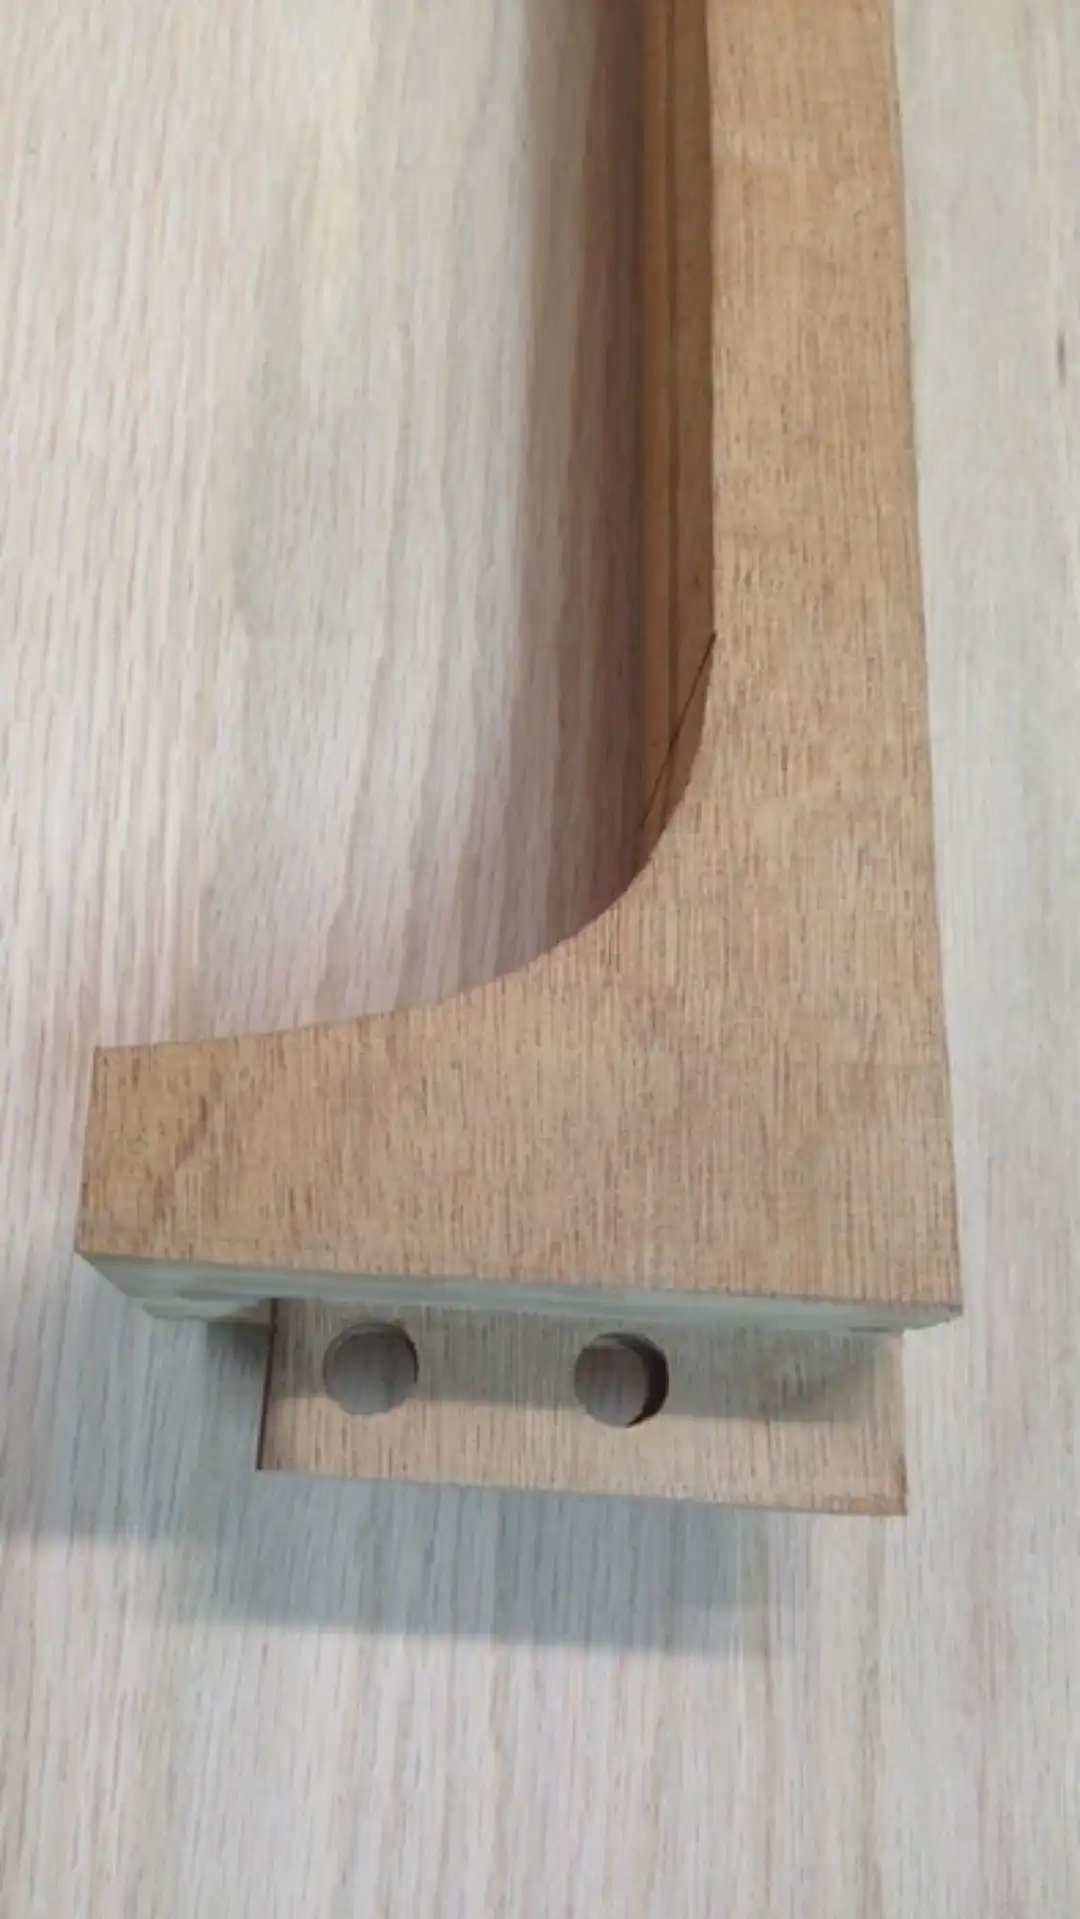
The tenon fits tightly into the mortise, and the bolts secure the neck in place, snug up against the body.

Completing the Neck
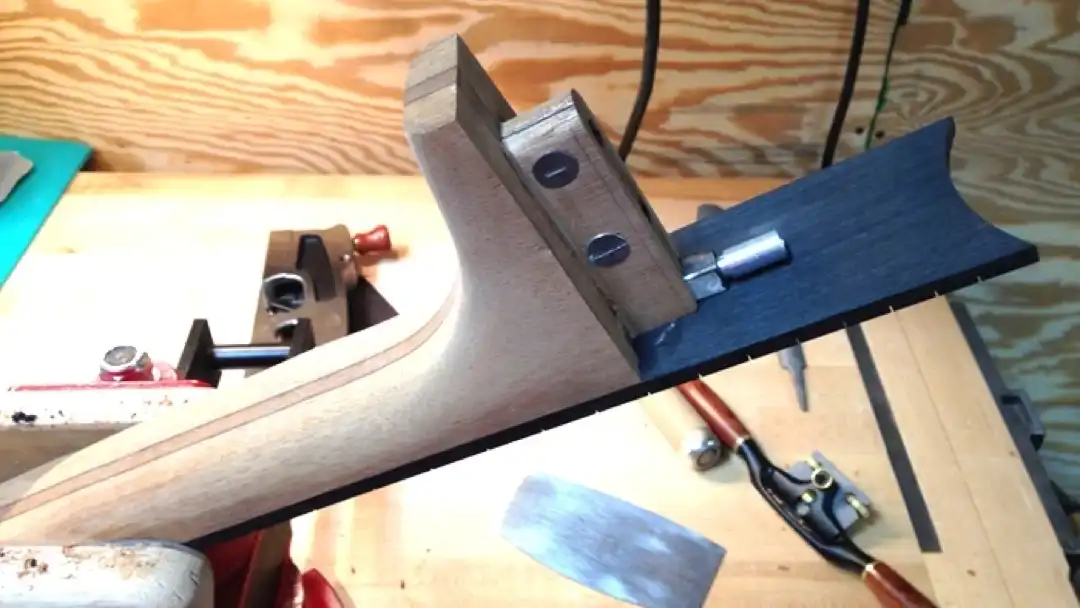
With the truss rod secured in the slot, the fingerboard is aligned and glued to the neck. The neck is shaped and dimensioned using nothing but hand tools. A coarse rasp does the rough shaping, a file shapes the curves, and a spokeshave smoothes the straight lines.

Sharp tools and patience.
Decorative Purfling
Did you know that decorative purfling can be added AFTER the body is bound?
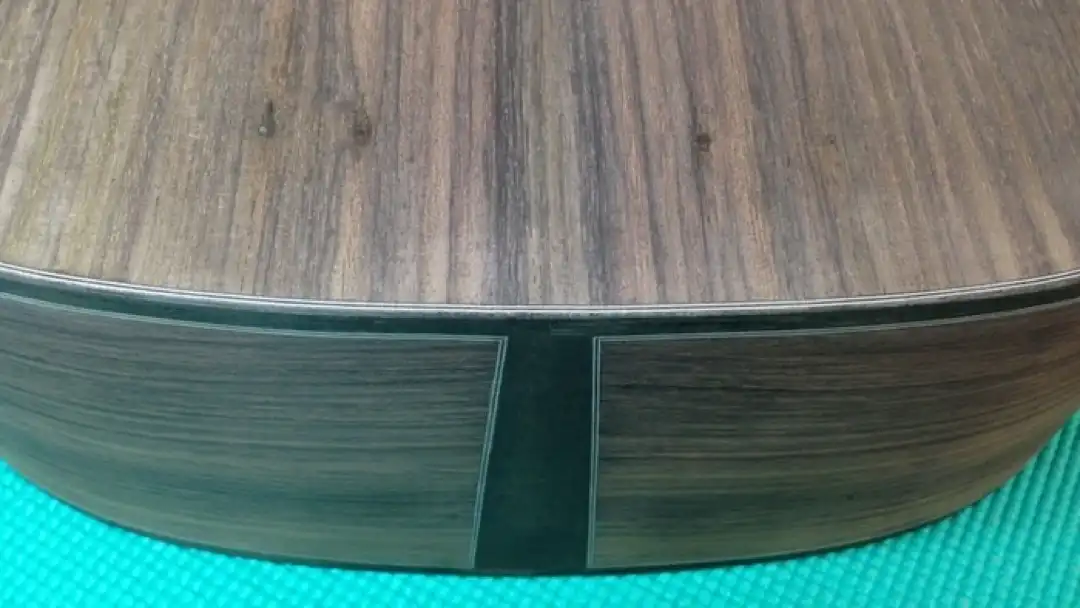
In the case of this guitar, I bound the body with super black Gabon Ebony (next to impossible to bend without breaking, but so rewarding when you pull it off). I had received a supply of pre-cut strips several years earlier. These slender pieces of Ebony had no purfling attached.
I believe that this was my second-to-last instrument bound using this the Ebony from that lot. I cycled through several other woods in the years following and, by the time I returned with a request for more Gabon Ebony, I got brown strips, not black. You probably know the rest of the story.
Purfling is not required and, at times, it is not even desired. But I wanted that look for this guitar. So I added it. Granted, it is a precision operation, but it is straightforward to achieve.
Back when I first pioneered my purfling-after-the-fact process, I had Whiteside build me a cutter for the task. Mounted in a trim router, and referencing the soundboard and/or the back, a groove is cut that spans the seam between the binding and the side. Care must be taken at the end graft, where I switch to a Dremel and hand tools.

The Headstock
The Ebony headplate is glued on to the headstock and shaped to follow the existing contours.
Another trip to the bench with the jeweler’s saw, and my spiral “C” logo is cut from Paua shell, traced onto the headstock and inlaid.
It is definitely easier (and less stressful) to inlay a headplate before it is glued to the headstock. However, perfectly locating a pre-inlaid headplate during glue-up presents its own challenges.
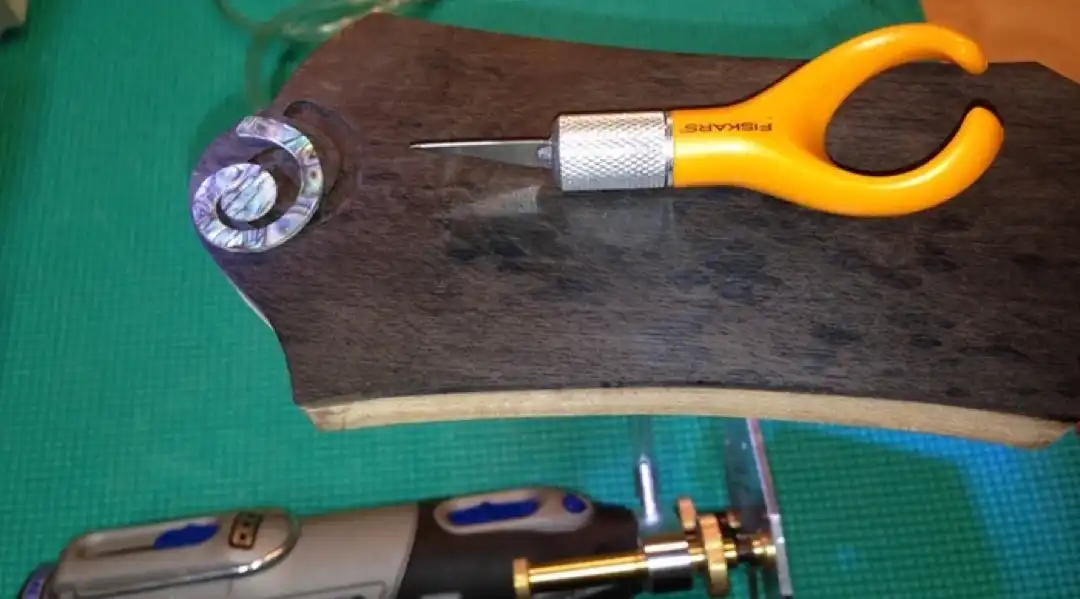
The headstock is drilled to accept the tuners. Employing an aesthetic enhancement I learned from Kent Carlos Everett, a shallow recess, slightly larger than the tuner washers, is also drilled to house the washers and nuts. Typically, machine head washers and nuts sit atop the headplate. Slightly insetting the washer and nut adds a distinctive visual element.

Recovering From Damage
When I was moving the body of the guitar in preparation for finishing, I {cringe} ended up with a sizable ding in the cedar top. I attempted to steam out the dent, but the appearance was distasteful.
Plan B: Make the damage go away! I proceeded to decorate the soundboard by adding inlay to the upper bout, incorporating the area of the dent.
I cut a few more Mahogany vine and Paua florets for inlaying the soundboard. The vine will appear to curl off the fingerboard and onto the upper bout of the body.
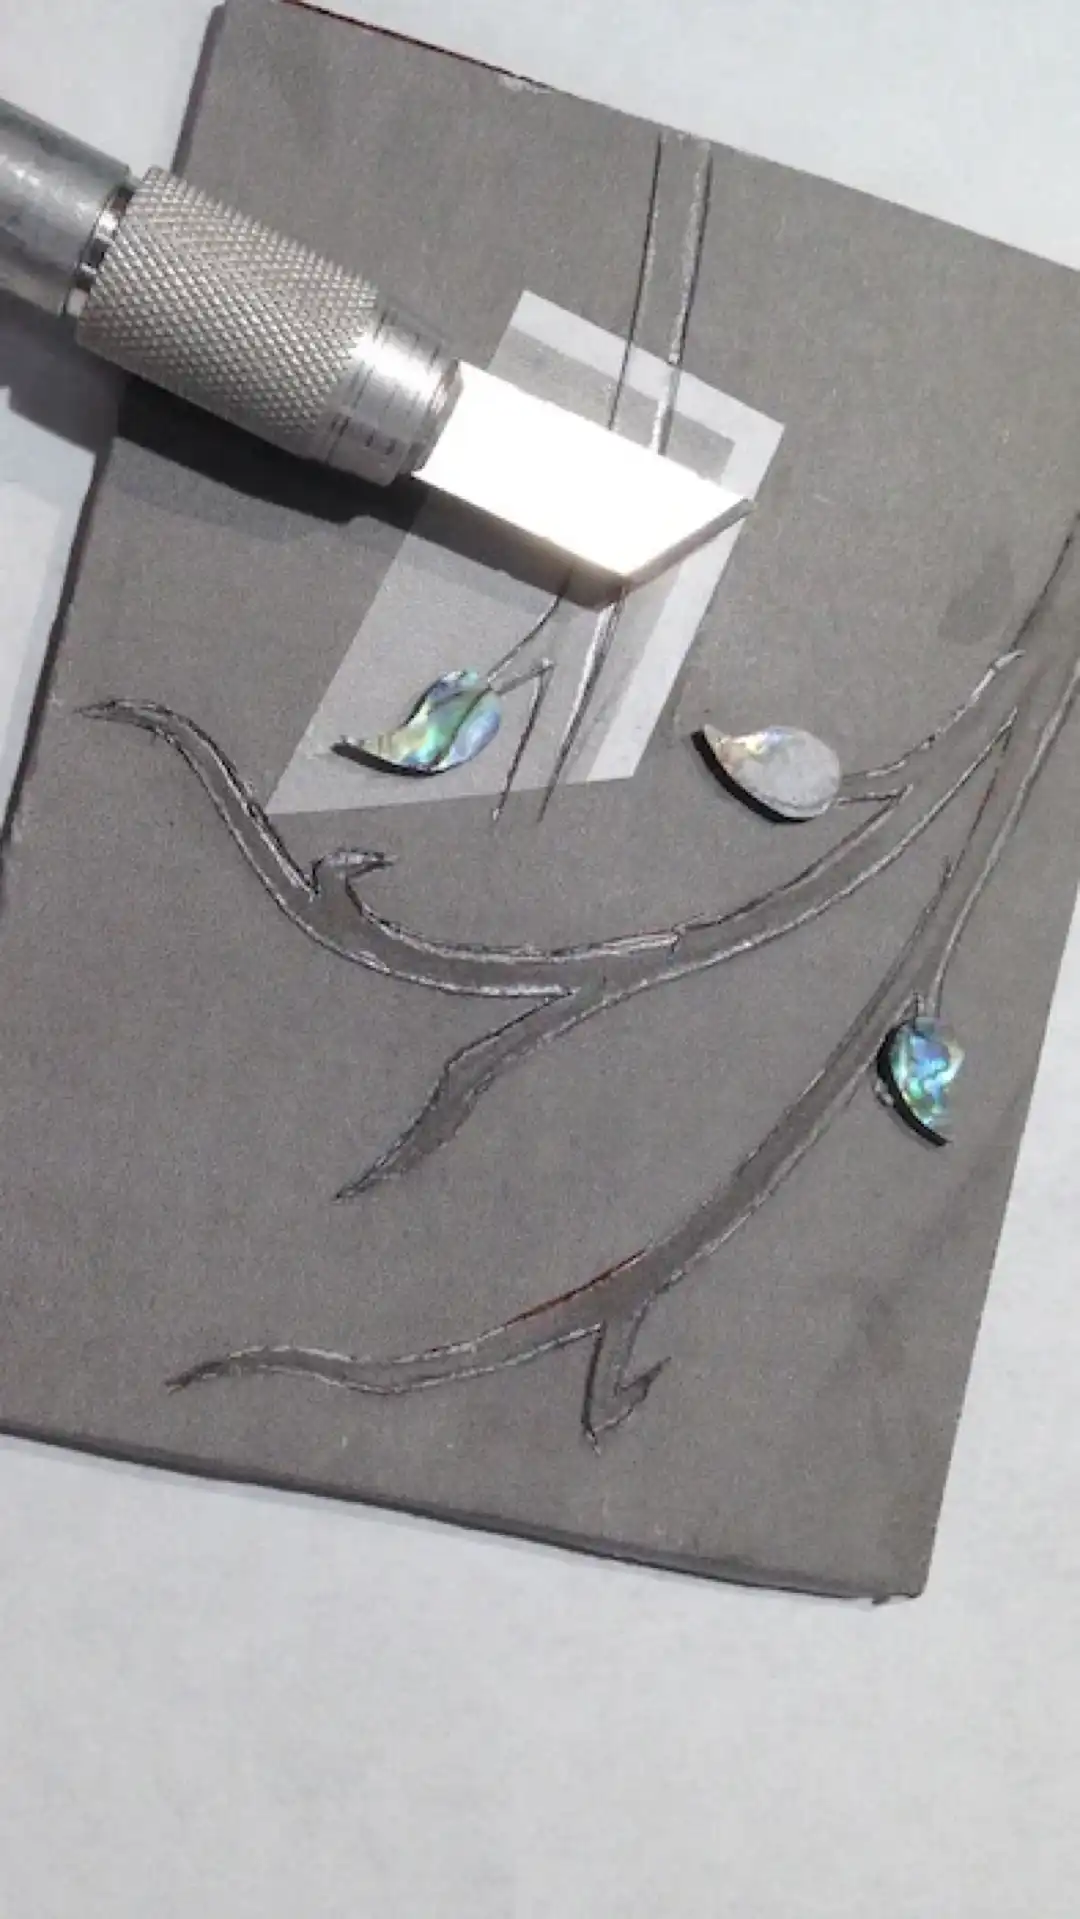
Note to self: Please be more careful, next time.

The Bridge
The bridge was fashioned from a piece of Ebony (coordinated to match the fingerboard, headplate and end graft). Measurements were calculated and the soundboard was lightly marked where the bridge would be manually positioned and glued.
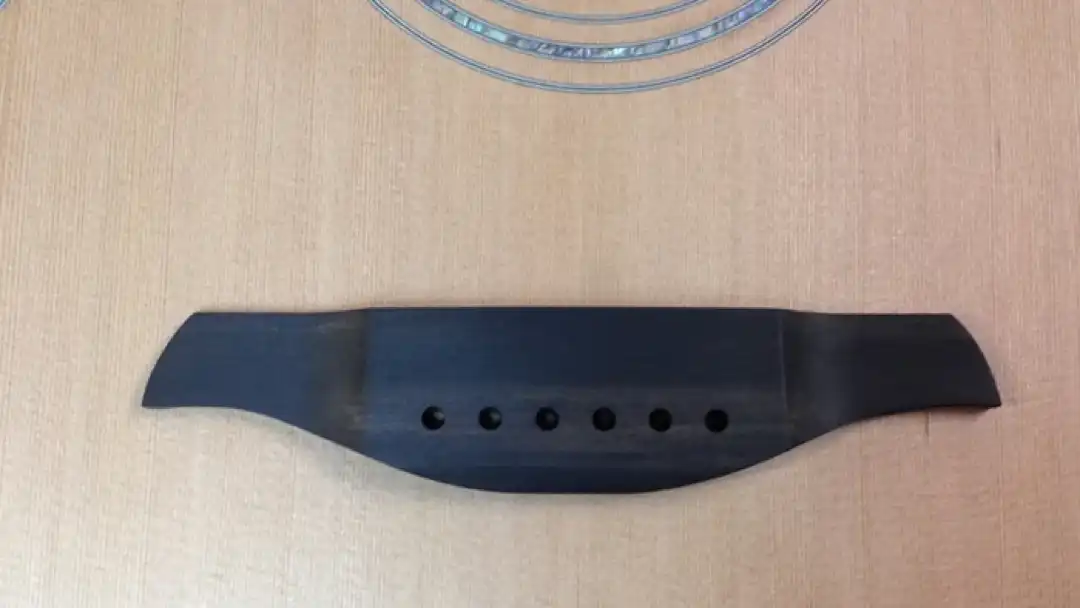
A pinned bridge can be temporarily secured to the soundboard using a clever tool called an acoustic bridge bolt. Two (2) flat head brass bolts, center-drilled through their length, are used to hold the bridge on.
If you are willing to drill all six (6) holes through the soundboard the guitar can be strung up for a sound test prior to finishing. Note that there is very little, if anything, that can be done about it at this point if you don’t like what you hear, but it is a clever way to sample what is coming!

Having dreadnought depth in an OM package, meet my East Indian Rosewood and Western Redcedar Continental.