Sometime around 2012, I saw one of the early all-Koa Taylor Grand Orchestra models hanging high on a wall in a Guitar Center on the West Coast. I asked if I could hold the guitar, which resulted in a scramble of employees moving amps and cases, and wheeling in a large ladder, all in an effort to satisfy a potential customer. It was fun to be a participant, and everybody did a great job. I purchased that instrument that day.
The Taylor proved to be a delightful guitar. The size, shape, weight, playability, etc. all came together in an excellent package. The designers and builders that played a role in the advent of that model have my respect. The overall look and feel of the Taylor Grand Orchestra inspired me to return to my shop and build the Canon.
This is not a "How To Replicate a Taylor" article, nor is it a "How To Build a Better Taylor" hit piece. Instead, I simply share some insight into what an all-around, excellent acoustic guitar inspired me to build, and how I went about doing that.
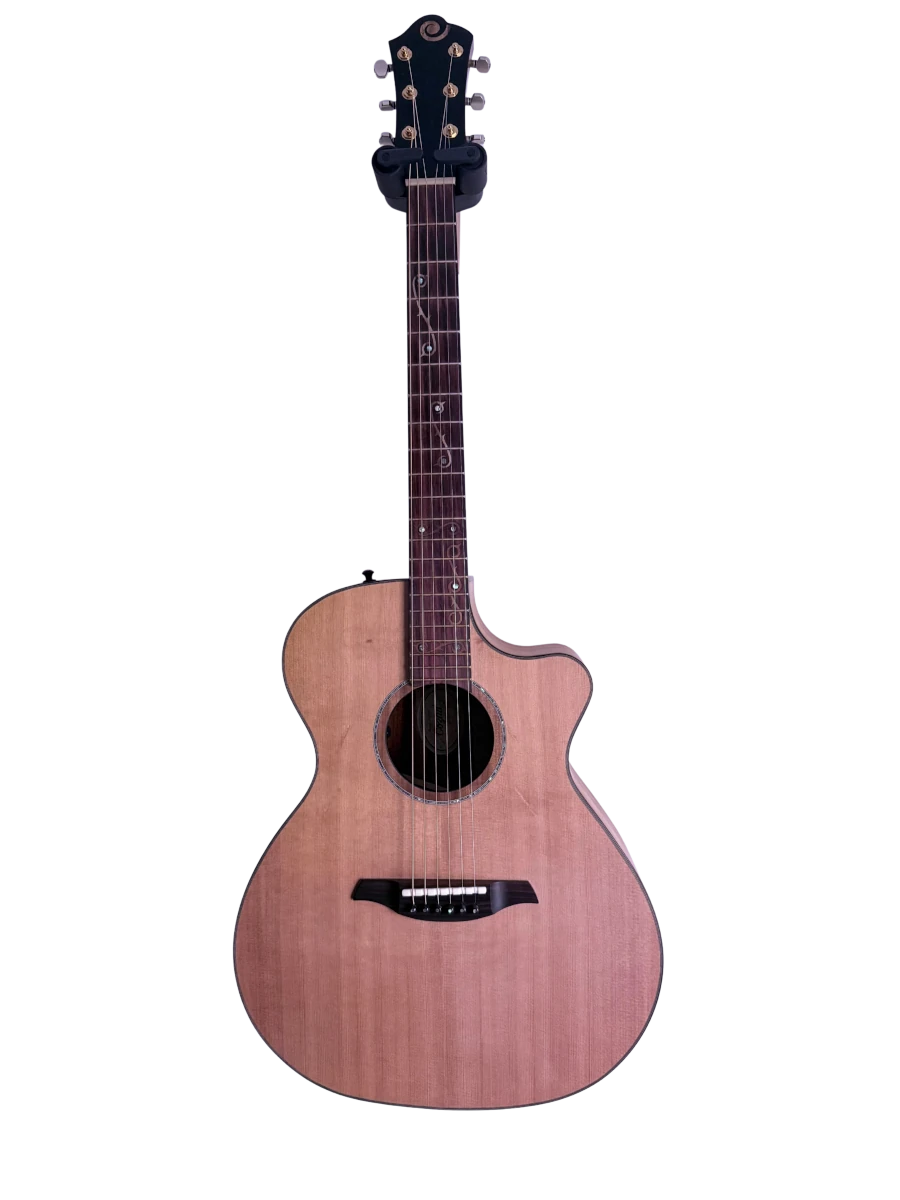
My goal for the output of this guitar was to produce a classic "slightly scooped midrange" frequency response, but have much more power from the low end. I incorporated Rosewood into the bracing and splayed the lower bout legs of the X a bit more.
On this page
- Specifications
- The Back and Sides
- Back and Side Bracing
- The Soundboard
- Binding and Purfling
- The Neck and Fretboard
Specifications
- Model: Canon
- Body Style: Grand Auditorium (Small Jumbo Venetian Cutaway)
- Upper Bout: 11.75″
- Waist: 9.5″
- Lower Bout: 16″
- Body Length: 20″
- Body Depth (Tail block): 4.5″
- Body Depth (Neck block): 4.0″
- Scale Length: 25.4″ (645 mm)
- Nut Width: 1.75" (45 mm)
- String Spacing: 2-1/4"
- Soundboard: Sitka Spruce
- Back and Sides: Oregon Myrtle
- Bracing: Laminated Adirondack Red Spruce and East Indian Rosewood
- Bracing pattern (Back): Progressive Splayed
- Bracing pattern (Soundboard): Conventional X
- Binding: Ceylon Ebony
- Soundhole Binding: Ceylon Ebony
- Rosette: Oregon Myrtle
- Neck: 5-piece Mahogany
- Fretboard: Macassar Ebony
- Fretboard Inlay: Oregon Myrtle
- Headplate: Gabon Ebony
- Bridge: Macassar Ebony
- End graft: Gabon Ebony
- Tuners: Sperzel Open-back Trim-lok
- Weight: 4.35 lbs (with tuners, strings, and pickup)
The Back and Sides
I built a more rigid, reflective back and sides, as opposed to a more flexible, "responsive" back. I wanted to use a relatively neutral tonewood that wouldn't steal all the credit for the perceived overall sound of the guitar, and I wanted the back and sides to be visually interesting.
I chose Oregon Myrtle for the task. The piece I selected for this particular guitar exhibits pleasing striping and has a visually interesting spalted heartwood appearance down the center.
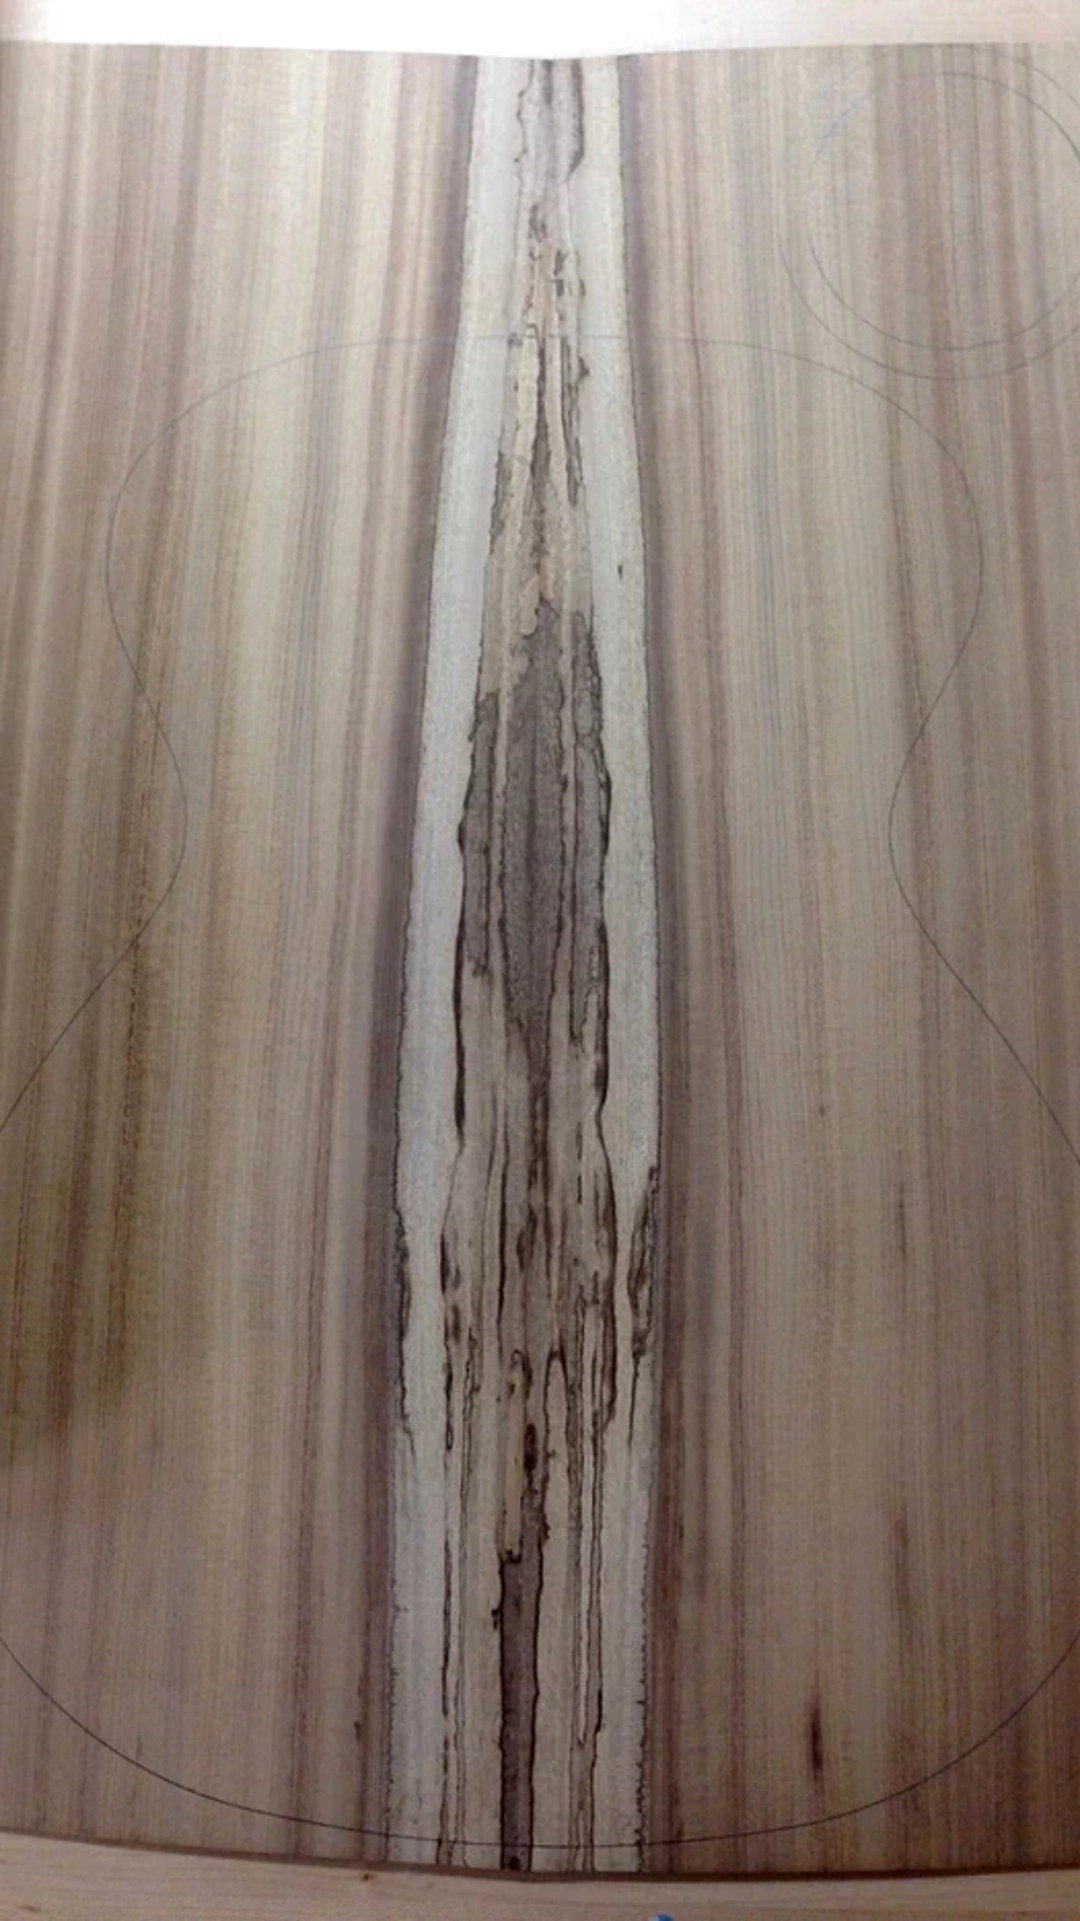
As pretty as spalted wood can be, it is the result of fungal decay. The hardness of the wood can range from seemingly unaffected to "punky", where it is so soft you can scoop it out with your fingernails.
I took a few extra few minutes to saturate the back and side wood with CA to overcome any weak spots.
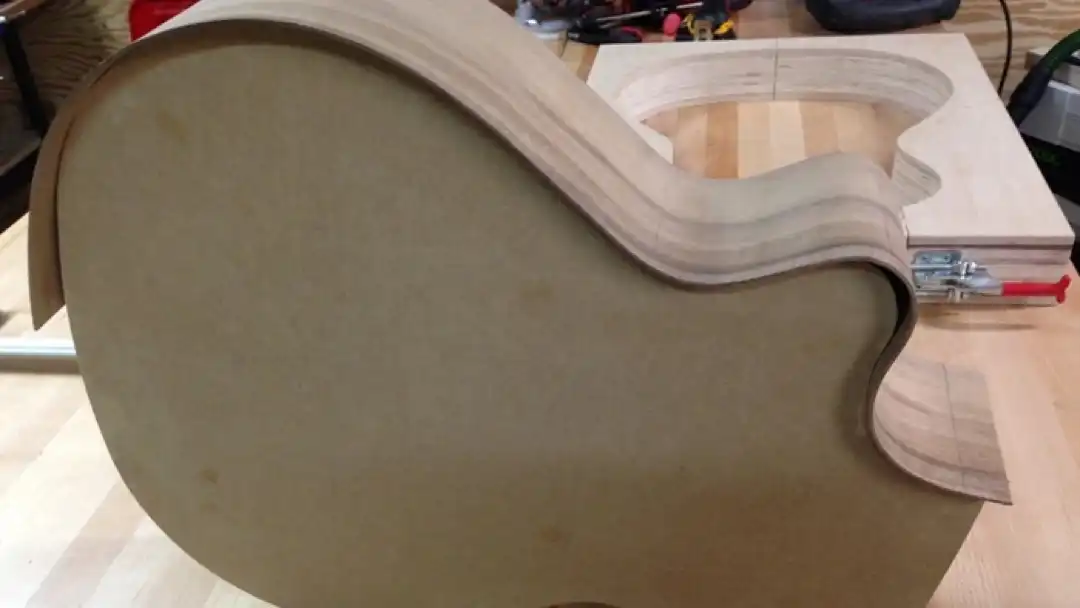
I bent these solid wood sides on an electric Side Bender.

For determining the shape of the cutaway side, I rely heavily on my bending forms. Think of them as the small, round "doughnut holes" that they stamp from the center of the dough. My bending forms are similar to what would be removed from the inside of the guitar body mold. I construct them separately using MDF to serve as both a model during the bending process as well as a clamping base.
Should you decide to employ a bending form, consider the dimensions involved: It should be the size of the body mold less the thickness of the sides. Do Not simply trace the corresponding body mold or soundboard template, or you will end up with sides that are too large. While you may be able to force them into your mold, you would be introducing undesirable stress on the instrument.
Using an iterative process of bend a little, fit a little, I am able to produce a very stable bent side, as I did with this guitar.
Bending Ebony successfully (without breaking) is challenging enough, without also having to deal with excessive springback. It is a bit more tedious, but I have had good results holding the bent binding tightly in place against a form after bending, and allowing it to rest overnight.
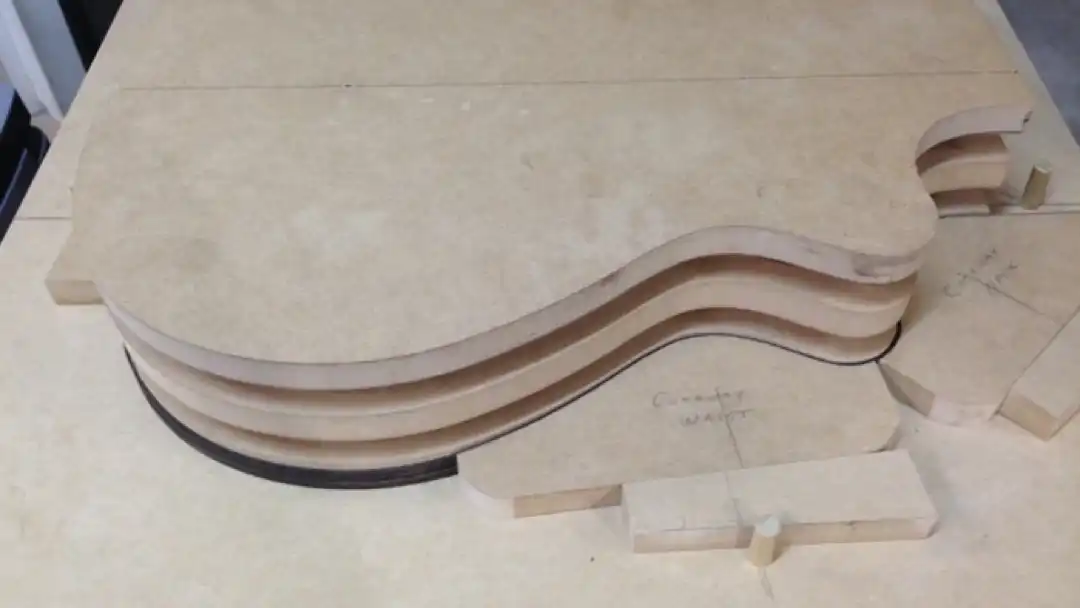
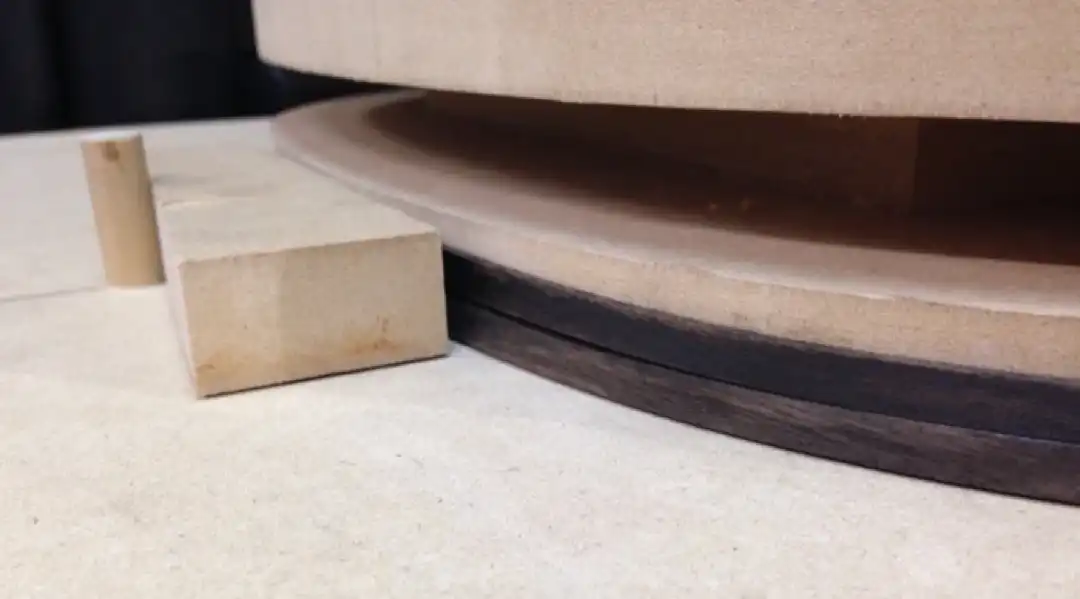
Bent sides are held in place in the body mold where they will (typically) reside for the duration of the body construction. Both the tail block and neck block are cut, shaped, drilled and glued onto the sides.
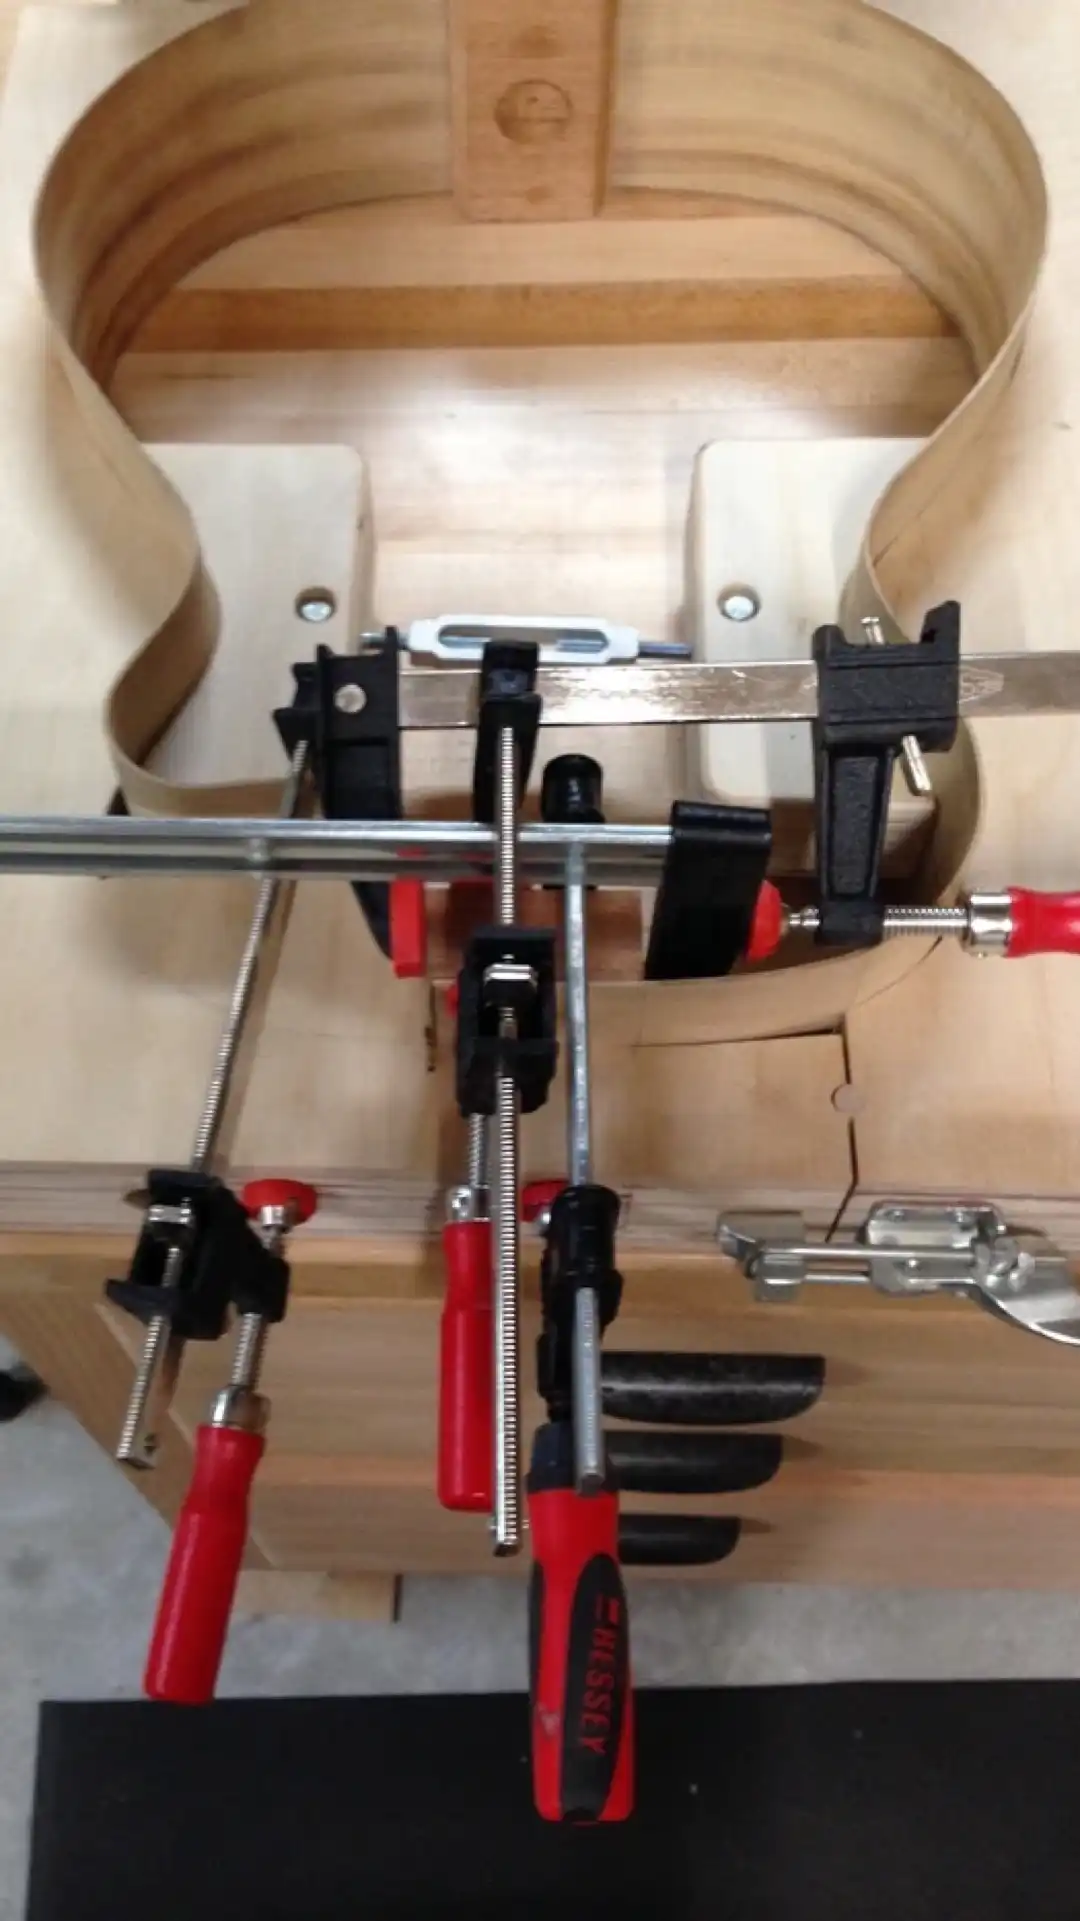
On the occasion when I will use kerfed lining instead of solid linings, I prefer so-called "reverse kerfed lining", a style of lining where the saw kerfs are glued to the sides, leaving a smooth, unbroken lining face exposed to view. Per a technique I learned from Kent Everett, I "pre-form" the fragile lining prior to attaching it.
Each strip is lightly wet (not soaked) and clamped "inside out" around the outside of the rim of the sides or, in my case, one of my bending forms. Additional cuts are made at the cutaway to allow for tighter bends.

After the lining has thoroughly dried, it is glued into place along the inside rim of the sides.

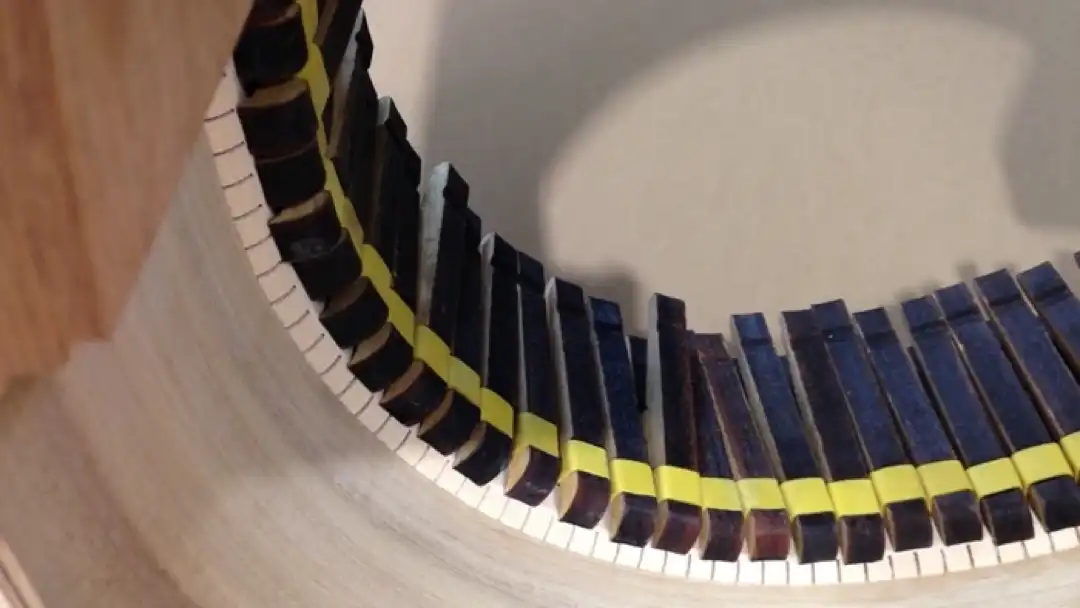
But for the use of reversed kerfed lining, the result was a fairly traditional acoustic body shell.

Back and Side Bracing
I fashioned a laminated brace, a combination of Rosewood and Adirondack Red Spruce. In addition to a next-level stiffness-to-weight ratio, the timbre of these braces is distinct from all-Spruce bracing.
I included a primary transverse brace on both the soundboard and the back, formed by sandwiching Spruce between two layers of Rosewood. The balance of this guitar’s bracing, the majority of pieces, was constructed by sandwiching Rosewood between two layers of Spruce.

When dry, the laminated product gets ripped back into individual braces. The process then continues as it would with common Spruce-only bracing, with extra care being afforded while shaping to avoid the cross-grain tearout.

I glued the braces to the back in a fanned pattern resembling the open fingers of the hand. This pattern results in a relatively stiffly braced back, which produces a resonance that is noticeably higher than that of the soundboard.
A note on brace shaping: A common approach to shaping braces involves gluing on rectangular sticks and, using a chisel, contouring those rectangles into their finished dimensions.
If there is a downside to this approach, it is related to the use of that chisel. To mitigate "splitting" already glued-on braces (a "no-no"), you need razor sharp chisels. If you "slip" with one of those razor sharp chisels, it is easy to gouge the soundboard, or worse.
Another approach routs or sands the basic contour(s) into the bracing prior to assembly. The braces may then be further reduced in size by sanding or planing with miniature tools.
Sanding a brace surface laminated together with a hardwood presents a color exchange challenge, where the oily dark wood dust is staining the lighter softwood. This can be overcome by using a scraper for the final pass.
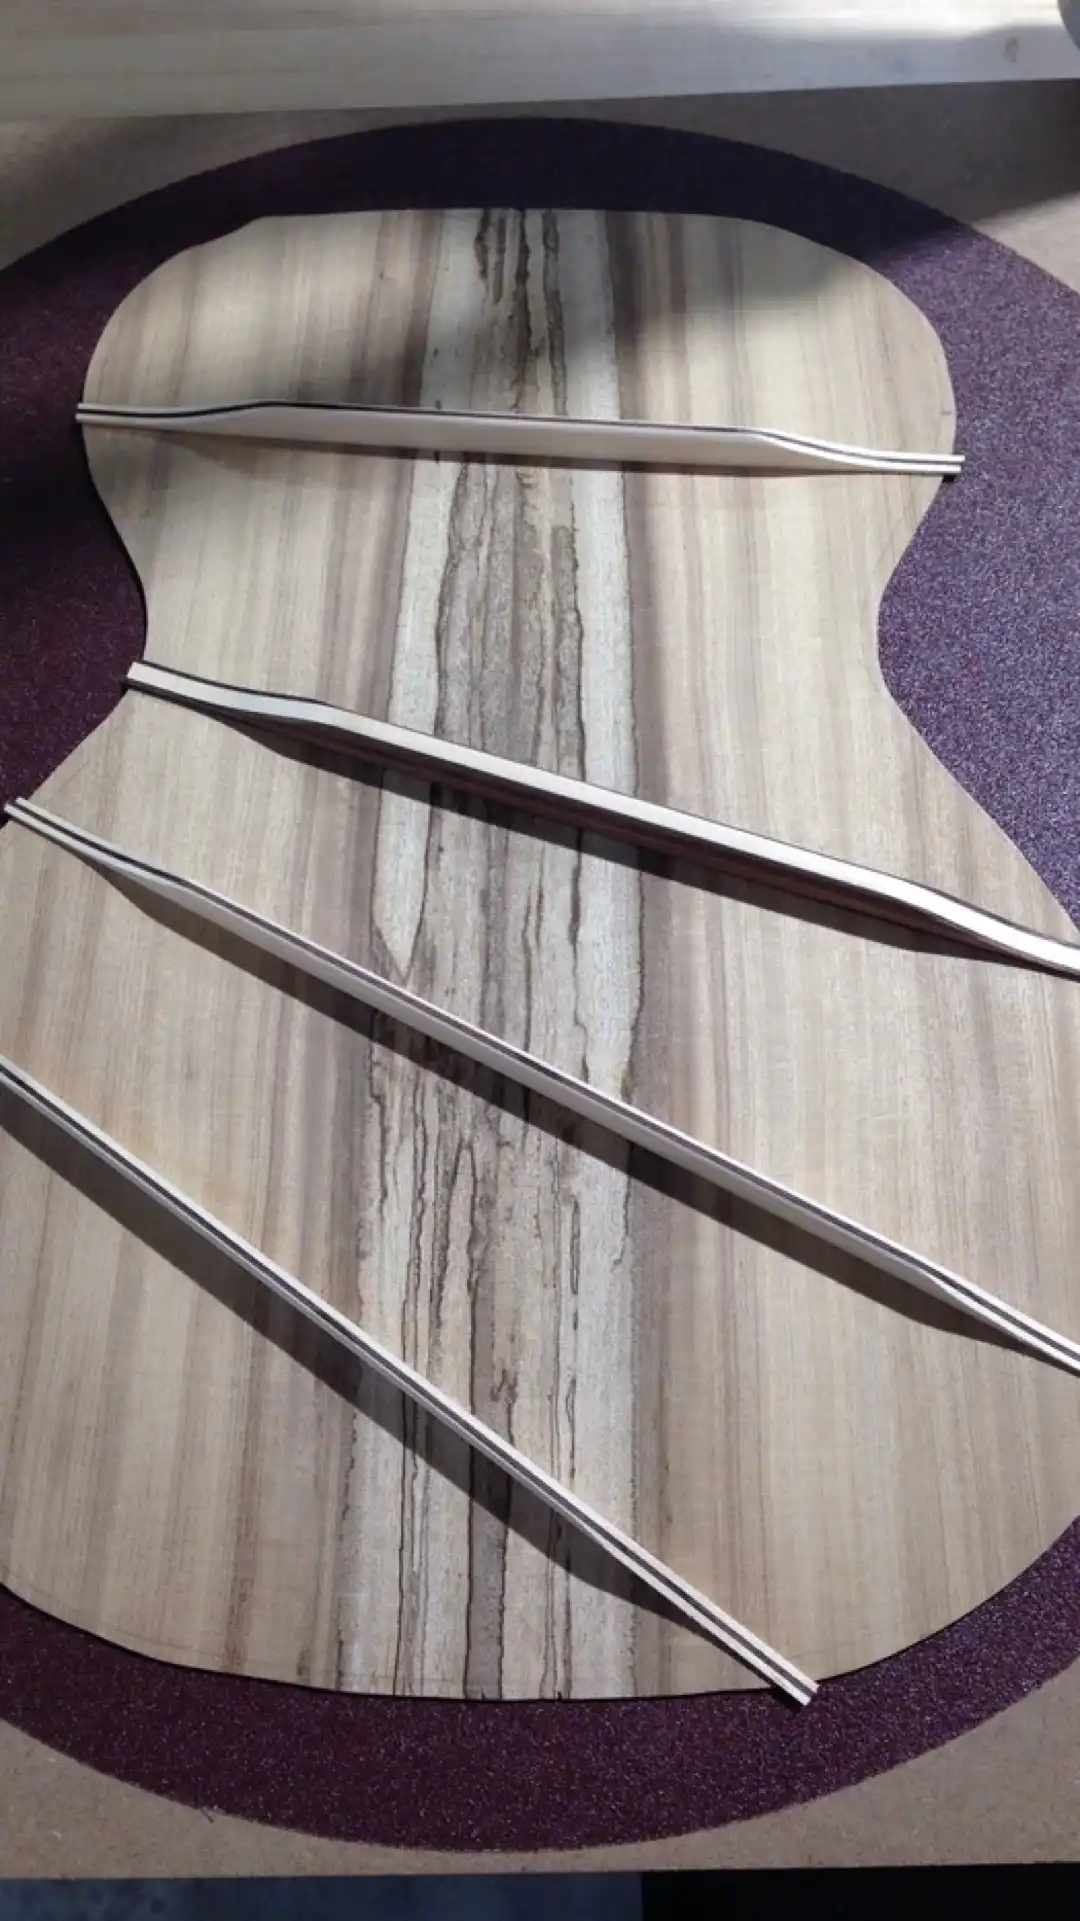
The back is glued to the sides, having carefully notched the kerfed lining to receive the thickness of the bracing at the edges. I opted to rest the braces on the ledge formed by the lining at the sides, akin to a joist resting on a wall.

I added small braces to the sides at the position of the back braces. These act to support the sides and, as with the ubiquitous reinforced tape of yesteryear, minimize the risk of the sides splitting along the grain. I subscribe to the notion that side braces may also assist in transference of the kinetic energy generated by the strings to the back plate.

The Soundboard
The Spruce soundboard was routed to receive a Myrtle ring I had cut from an unused section of the back plate. Purfling was added around the outside edge of the ring to form a minimalist rosette.

Reinforcement was added at the soundhole on to the back (inside) of the soundboard. Traditionally, small braces and/or plates are used for this purpose. This guitar will receive a hardwood ring. This serves add reinforcement to a delicate section of the soundboard while also providing support for a wider soundhole binding.

Ebony, being particularly short-grained and brittle, is not an easy wood to bend. Nevertheless, it has been one of my favorite choices for binding. In recent years I have found Ceylon (Indian) Ebony to be much more forgiving when bending than Gabon (African) Ebony, and tend to use it more often.
I have a repeatable method for forming my binding prior to installing it around the soundhole.
First, I sand a strip of binding to approximately half the thickness used to bind the edges of the body. While this definitely aids in preventing breakage, I simply prefer the appearance of a thinner soundhole binding.
Next, I drop the piece of binding into a pot of simmering water. A minute or two in the hot bath is sufficient to relax the wood. I remove the now malleable strip from the pot, wipe away any excess water, and immediately inset the strip into a circle routed in a plywood form.
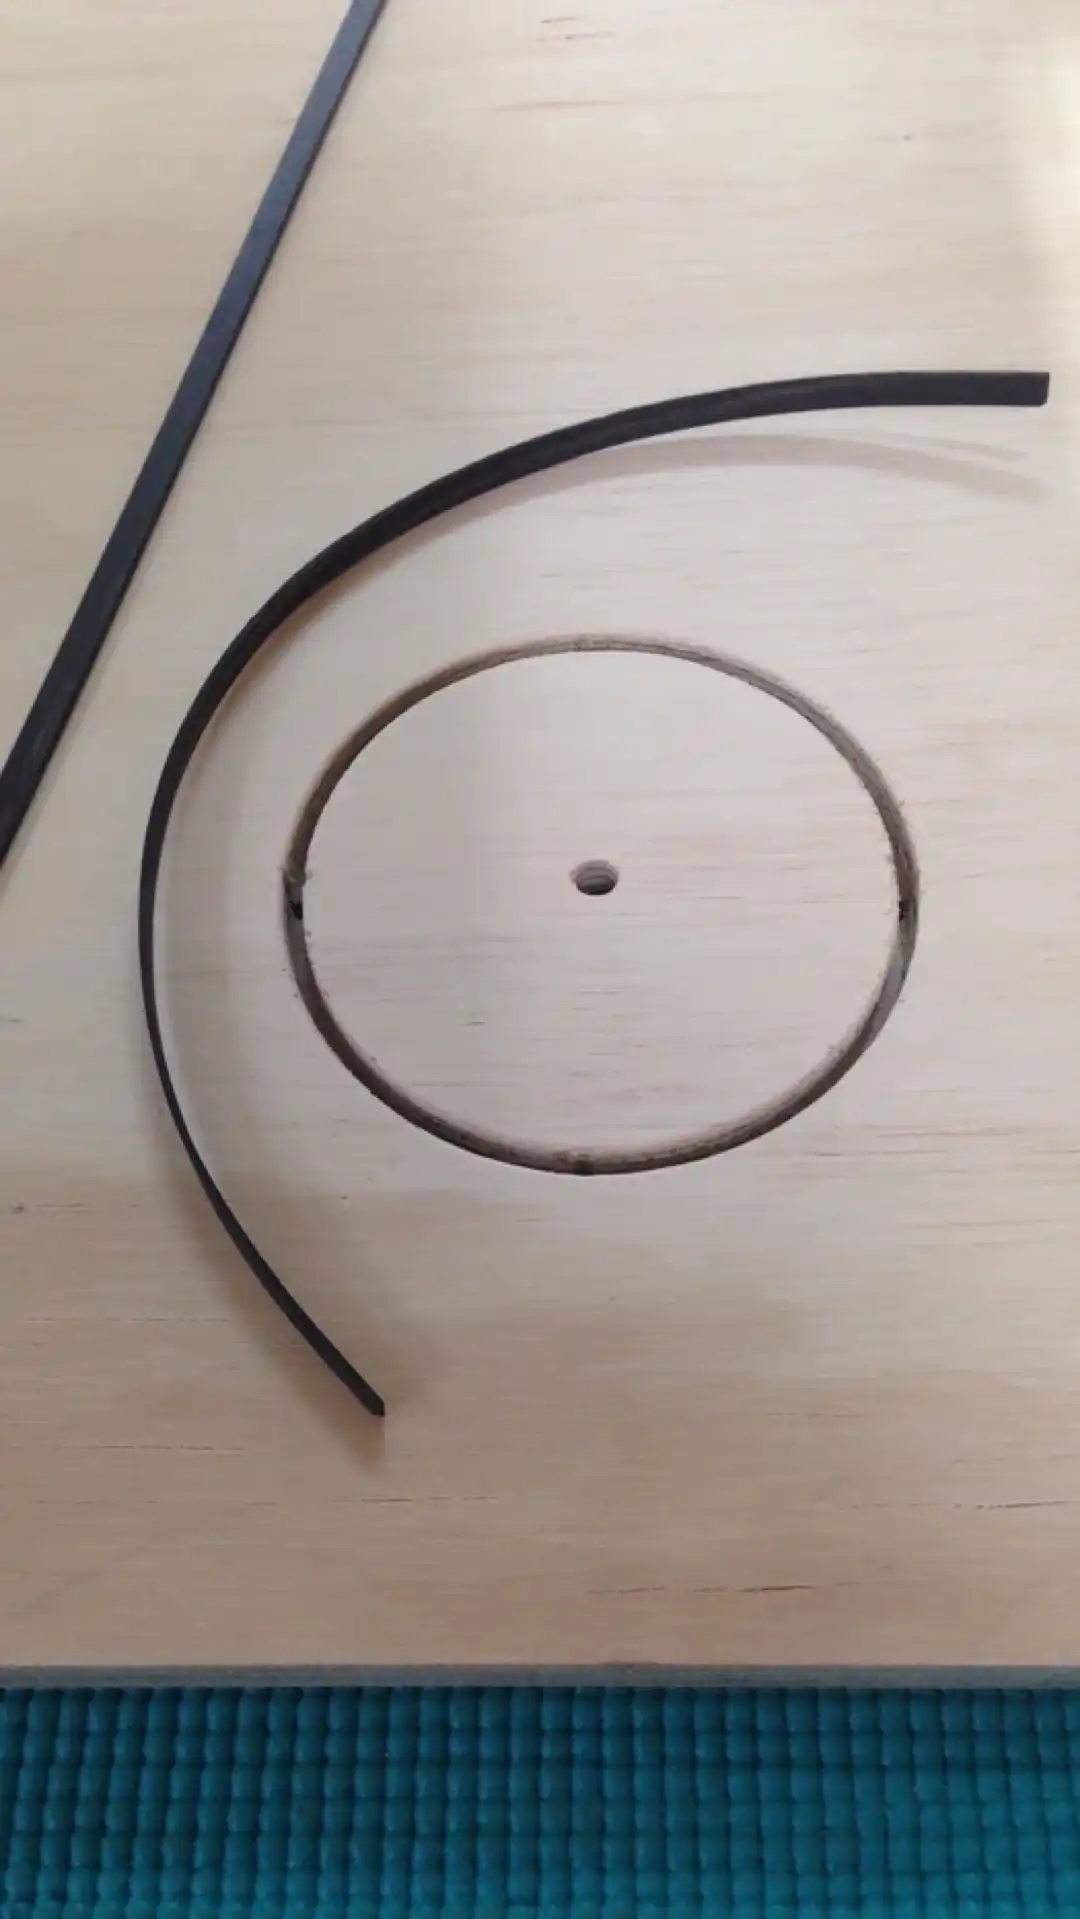
The routed channel is wide enough to allow the strip to overlap where the ends meet. This is left to dry thoroughly.

Cut to size and glued in place, the soundhole binding is a welcome visual addition.

I made use of epoxies, and I splayed the legs of the X-brace wider than usual. Rosewood plays a big role in shaping the sound. As a result, no one picks up one of these guitars and thinks they are "missing" something, soundwise, especially not from the low end.
I have fashioned fixtures that I use at the router table to rough out my contoured braces. They get positioned and glued in place on the go-bar deck.

When the glue is dry, focus turns to shaping and/or tapering, removing unwanted bracing material. I rely on sanding techniques more than razor-sharp chisels for this process, especially with laminated braces. The grain is going in all sorts of directions, and I can experience fewer surprises by sanding.
I am not removing brace material for fun. Nor am I shaping the braces in order to make them "look cool!" The primary role of these braces is to provide sufficient support to resist the forward rotation of the bridge due to the pull of the strings.
With that in mind, I set out to reduce the sound-deadening, or "damping" impact of unnecessary wood. If I remove too much brace material, the soundboard will suffer deformation under string tension. If I don't remove enough brace material, the guitar will never BE ALL IT CAN BE.
My goal is to eliminate as much bracing material as possible without compromising the structural integrity of the soundboard. When I get this "just right", and I pluck those strings for that very first time, I am instantly rewarded for my efforts!
My laminated bracing reduces the overall mass of wood typically needed to undergird the soundboard. Aesthetically, it is a clean look. Sonically,I find it quite stunning.

Binding and Purfling
After the soundboard is glued to the sides, the excess material around the exterior of the soundboard and the back is flush cut to the sides.

I added an Ebony end graft to the body, no purfling, and pre-drilled for a strap jack.
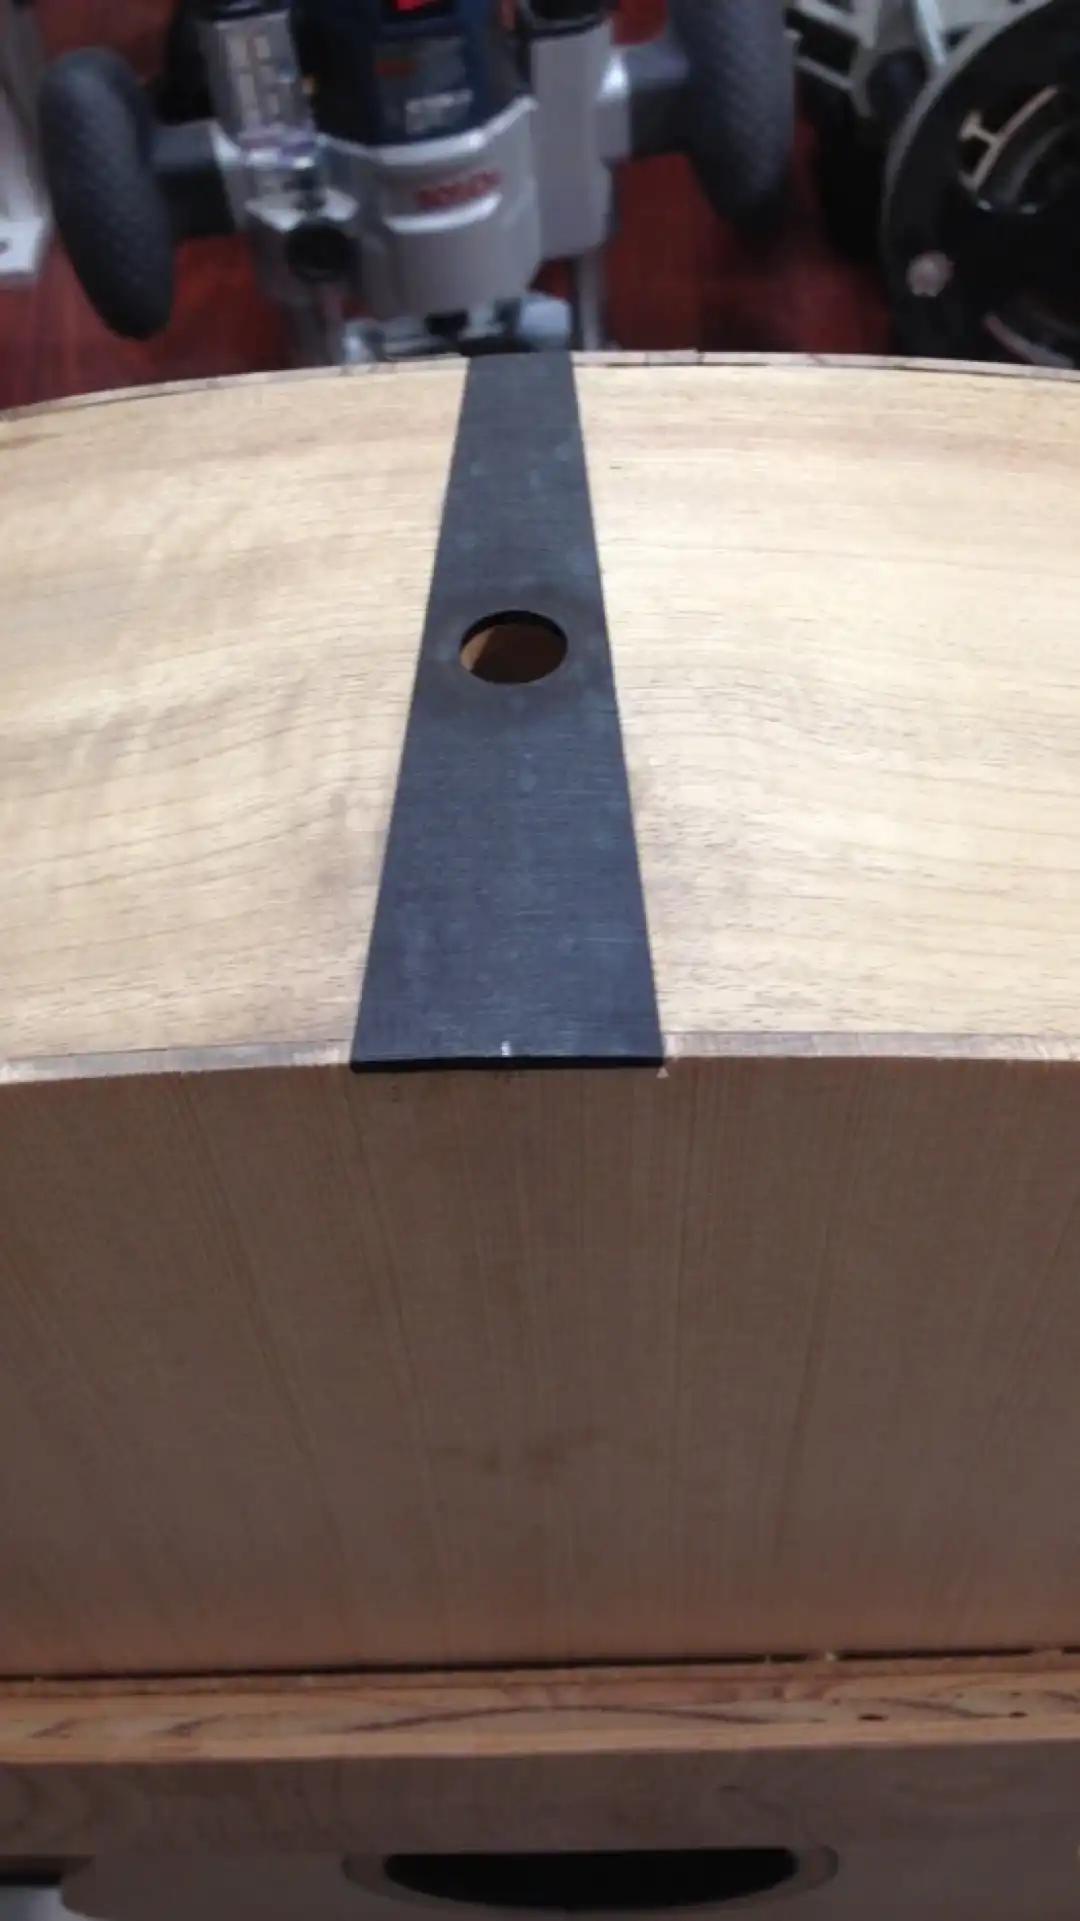
This body features a cutaway. I added a strip of binding where the cutaway meets the neck prior to routing the binding and purfling channels around the perimeter of the body.

Dried glue is removed and binding is carefully blended into the body using a scraper.
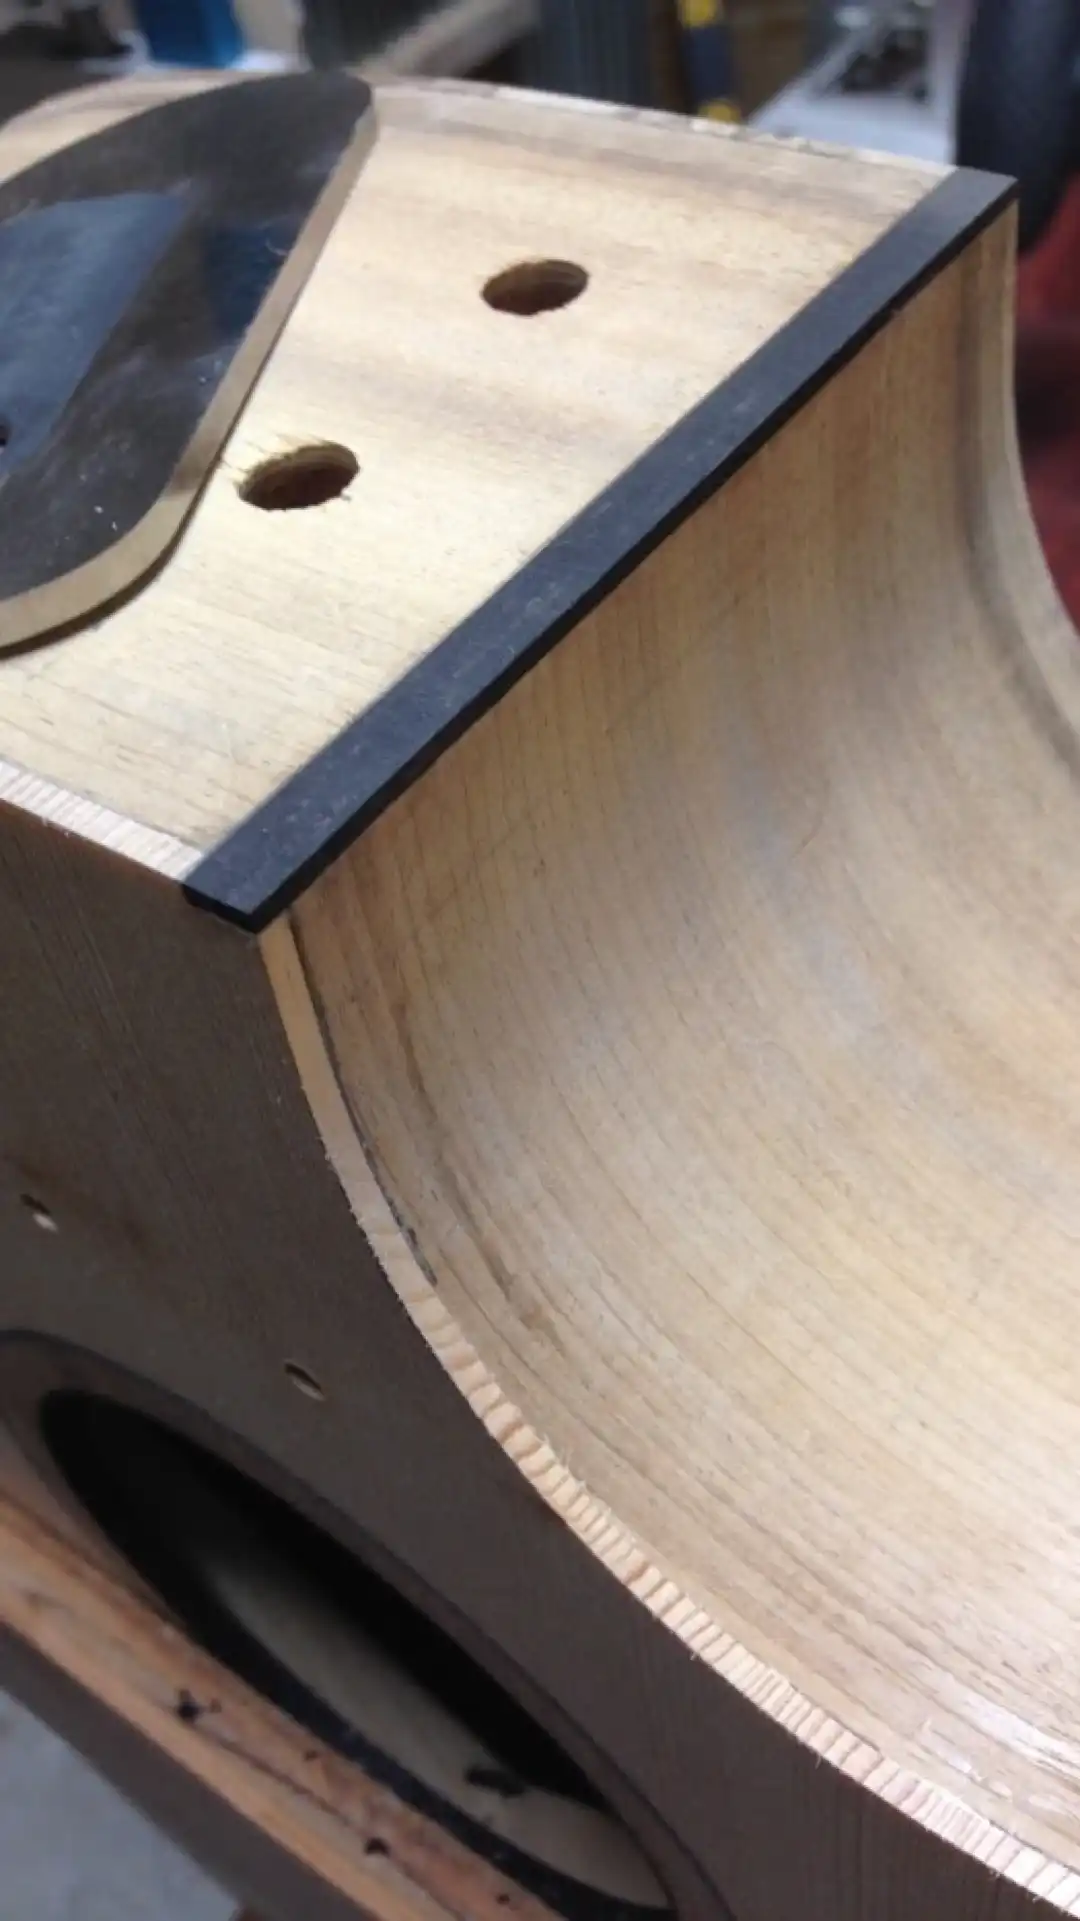
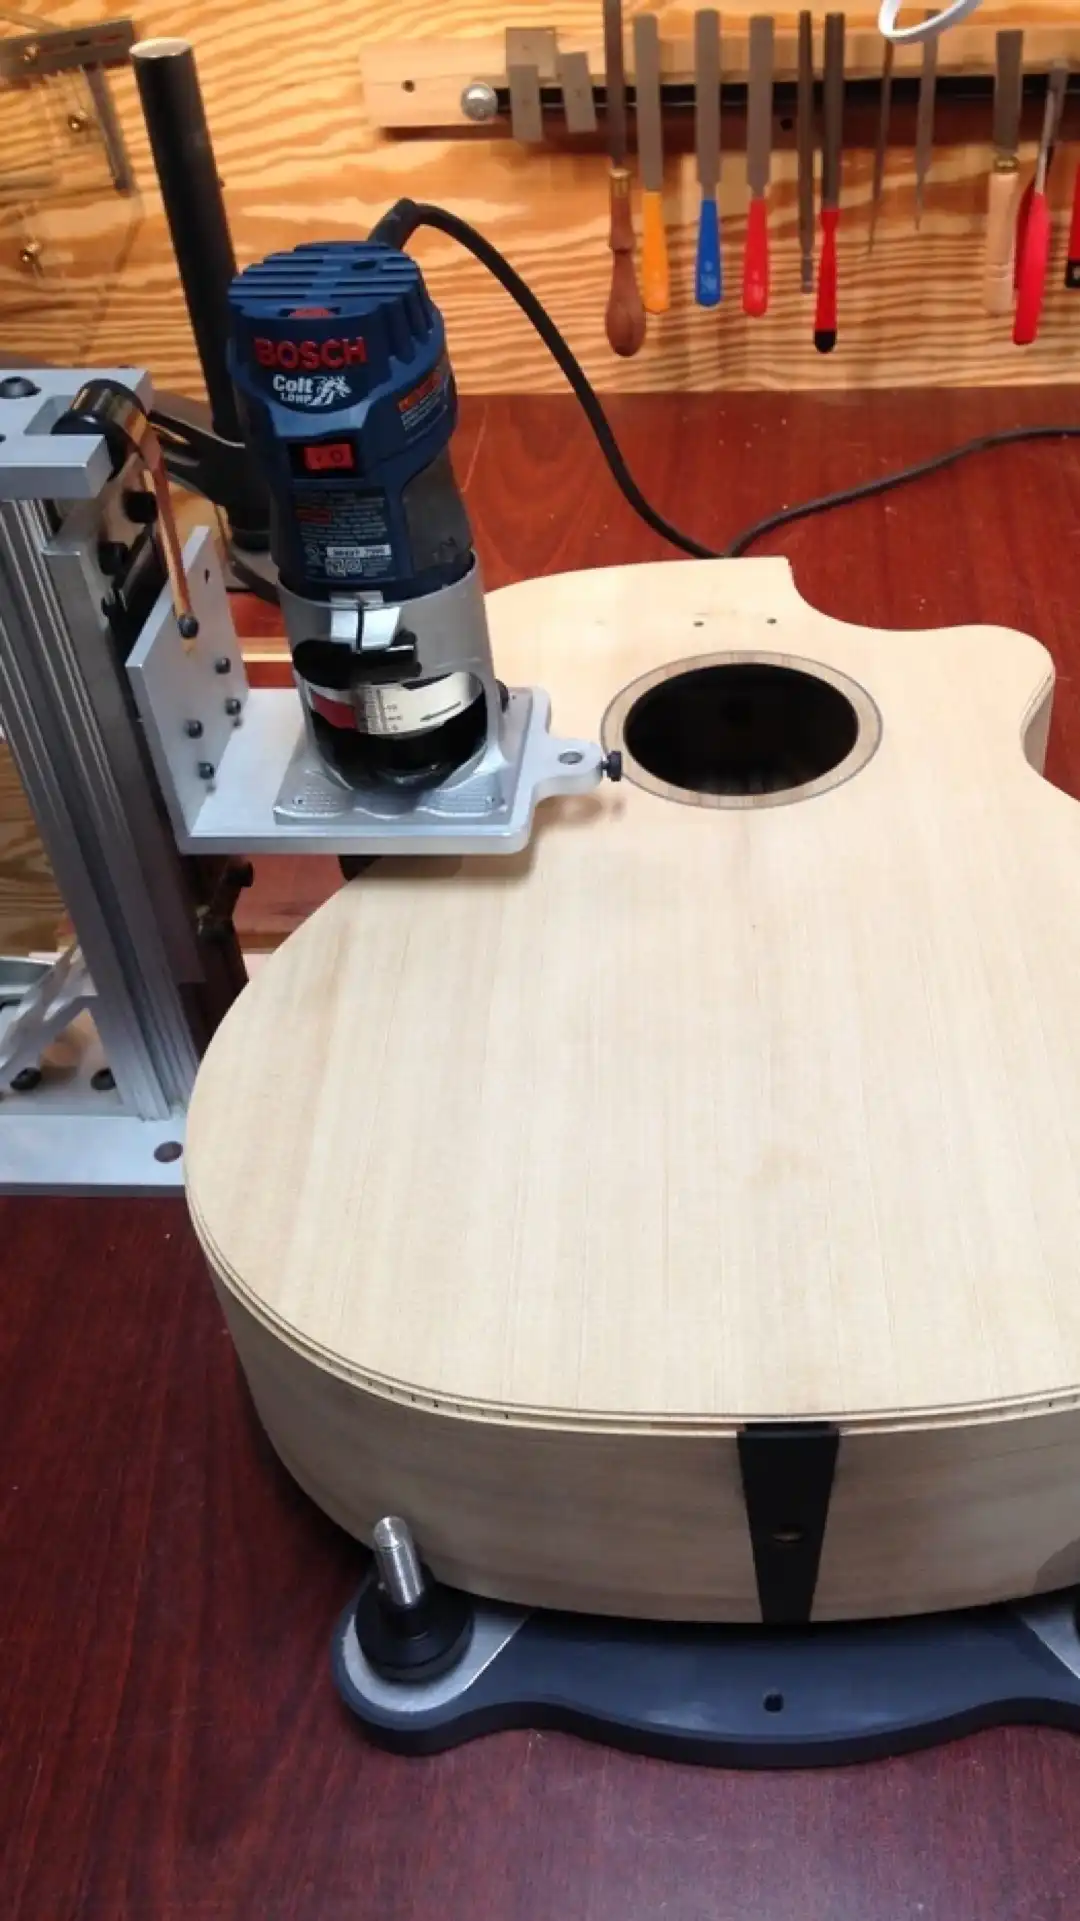
This body was mounted onto a sled, leveled, and rotated across a "tower-style" binding router, which glides on a vertical rail and is equipped with a depth stop. The process is effective for cutting binding and purfling channels into both the soundboard and the back of the guitar body.
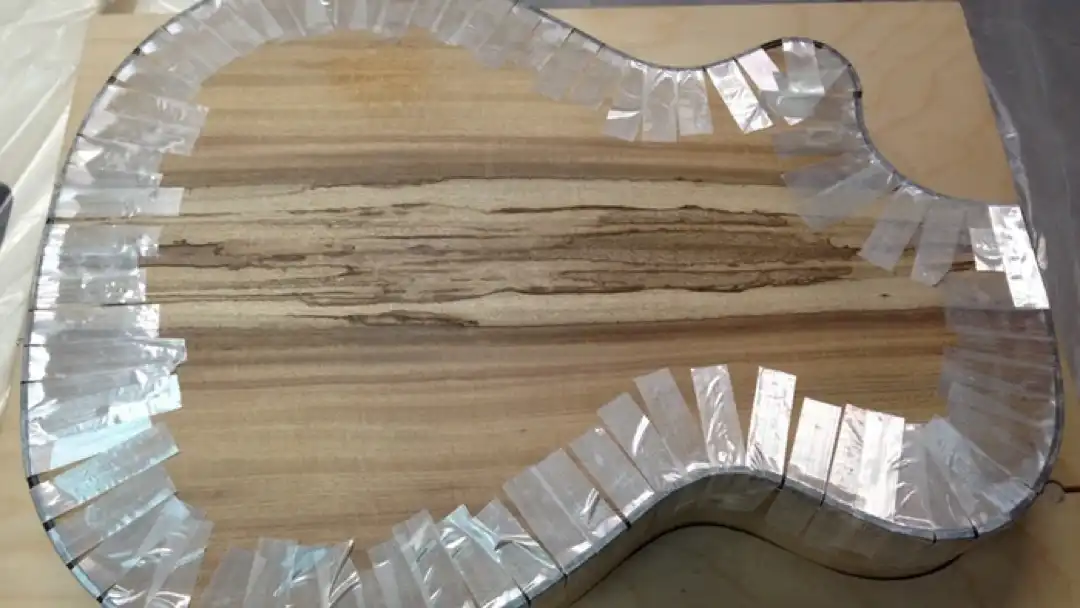
Mise en place - Staging materials is especially necessary when applying binding in the traditional fashion, where the purfling strips and binding are glued to the binding channels in one operation, all at once.
Tape holds everything tightly in place until the glue dries.
The Neck and Fretboard
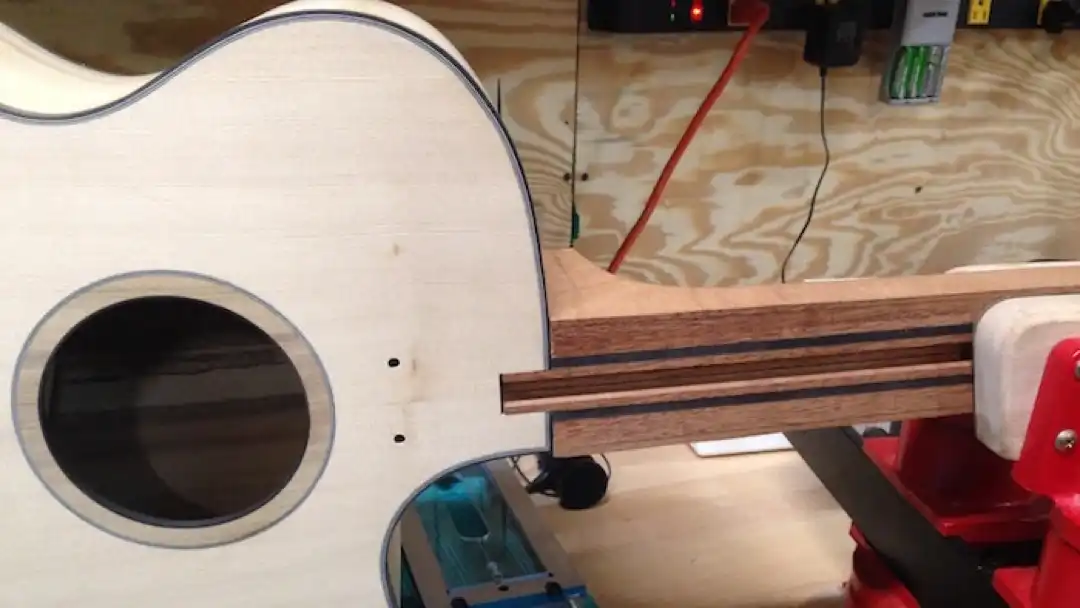
This 5-piece laminated neck included carbon fiber stiffeners. It was joined to the body with a mortise and tenon, being held securely in place with two bolts. A truss rod slot was routed down the center.
I had intended from the outset to inlay conventionally-placed, white shell dot fret markers and be done with the appointments. I recall that, as I was constructing the body, I began to envision a little something more. I set about to create what I saw in my mind’s eye. I drew the pattern on paper and, once satisfied, transferred it onto offcuts (waste sections) from the Myrtlewood back.

After installing the truss rod, the fretboard was glued to the neck. An aluminum fixture having plastic cauls was used to clamp the fretboard in place while the glue dried.

I shaped the neck and readied the guitar for finishing.

I finished the guitar with CA glue. That includes the headplate, the entire back of the neck, the soundboard, the sides and the back. The only components that didn't get any finish on them was the fretboard and the bridge,